Epoxy Resin For Tumblers

Epoxy Resin for Tumblers: How to Choose a Coating for Smooth, Even Coverage

Spin a tumbler under a shop light and it looks perfect. Tilt it, and a thick ridge shows up near the base. Another cup has gorgeous glitter but a rough patch around the decal. Pouring on more resin rarely fixes either problem. The coating, the decoration, the amount you apply and the turner all have to cooperate.

Good epoxy resin for tumblers spreads across the surface you want covered, stays workable long enough to finish the cup, and cures into a film that fits how the cup will be used. A trial on your actual cup tells you more than any clarity claim on the bottle. That goes for a one-person studio and a bulk buyer alike.

Below: which properties to compare, how to control coverage, and what to check before a tumbler epoxy resin goes into regular production.
Epoxy Resin For Tumblers

Pick a coating resin, not just a clear one

Two-part epoxy cures through a reaction between resin and hardener. On a tumbler, you want a controlled film over a prepared cup and its decoration. Filling a deep mold is a different job — the resin has to cure through a much larger mass.

So don’t grab a deep pour epoxy just because it’s clear and lets bubbles escape. Its working and curing behavior may not suit a thin film on a rotating cup. A tabletop epoxy deserves the same scrutiny: test it on a curved surface before you commit. A product’s category name is a starting point. It isn’t proof.

UV resin is a separate system altogether. Opaque glitter blocks the light it needs to cure. A UV product that works on a small, exposed detail won’t automatically coat a whole tumbler.

Viscosity: how far the resin moves and how well it stays put

Viscosity decides how a mixed resin spreads and how easily it travels while the cup turns. Very thin material wets out fast but can drift toward an edge. Thicker material holds position, but it may leave marks or fail to settle around coarse glitter.

No single viscosity is “best” for tumbler epoxy. Test the mixed resin at your real working temperature, over your real decoration. When a supplier quotes a number, ask three things: is it Part A, Part B or the mixed system, and at what temperature was it measured?

Temperature matters here too. A resin that behaves in a cool workshop may run in a warm production room. Keep resin and cups inside the supplier’s stated range. Don’t thin the mix with solvent, and don’t tweak the hardener to change flow — switch to an approved grade instead.

Working time has to match your real coating cycle

A fast-cure claim means little if the resin stiffens before you finish the cup. Your window has to cover measuring, mixing, coating, an edge check and any approved bubble treatment.

Look at how the pot-life figure was obtained. A lump of resin in a mixing cup behaves differently from a thin film on a cup. For planning, time it yourself: from the first mix to the last cup you can still coat consistently. That number is usually shorter than the datasheet figure.

Keep four stages separate — rotation time, handling time, recoat time and full cure. A cup that comes off the turner isn’t ready to pack or use. Faster grades can raise throughput, but only after you’ve verified each stage under your own conditions. [1]

Judge clarity and durability separately

Clear resin should let the design show through without haze. Compare samples over white paint, pale colors, metallic finishes and your darkest artwork. A dark cup exposes surface waviness that glitter would hide.

Clarity on day one says nothing about color stability a year later. Ask what testing backs a yellowing-resistance claim, then compare samples at equal thickness under the same light. “UV resistant” doesn’t mean the cup will never change color.

Hardness, scratch resistance and impact strength are also three different things. Glossy resin still scratches. A dropped cup can chip at the edge. Evaluate the finished, decorated cup — rim and base included — not a flat test chip.

Treat the cup and decoration as one system

Find out what the epoxy will actually touch: bare stainless steel, a factory coating, paint, sealer, vinyl, or the adhesive under the glitter. Adhesion depends on that top layer and on everything beneath it.

Follow both the blank supplier’s and the resin supplier’s prep instructions. Remove contamination, do any specified abrasion, clear the residue, and then keep skin oils and shop products off the prepared surface.

Let paints, adhesives, inks and sealers dry or cure the way their makers require. A surface that looks dry may not be ready, so confirm compatibility with a trial. Watch for decals that bleed, lift or trap bubbles under the epoxy.

Plan a clean coating edge. Keep the interior, threads, lid sealing surfaces and drinking-contact areas free of decorative coating unless the whole system has been assessed for that use. A generic statement about cured resin doesn’t replace documentation for your specific application.

Measure coverage — don’t guess from cup size

Capacity tells you how much a cup holds, not how much exterior it has. Height, circumference, taper, base shape and decoration all change how much resin you need. Two cups sold at the same fluid-ounce size can need different amounts.

For a roughly cylindrical wall, a first estimate is circumference × coated height × target wet-film thickness. Use square centimeters and centimeters, and the answer comes out in milliliters. It’s an estimating method, not a recommended film build.

Say the circumference is 25 cm and the coated height 18 cm. That’s about 450 cm² of sidewall. A hypothetical 0.2 mm wet film is 0.02 cm, which gives roughly 9 mL before the base and before losses. It’s an illustration only — the approved film thickness comes from the resin’s own instructions.

Glitter texture, taper, resin left in the mixing cup and application losses all push the real number up. Confirm by experiment and log the consumption per acceptable finished cup. If you buy by weight, convert with the supplier’s mixed-resin density. Grams and milliliters aren’t interchangeable.

Keep mixing and turning repeatable

Measure both components at the exact ratio and on the measurement basis the grade specifies. A volume ratio shouldn’t be dropped into a weighing procedure unless the manufacturer gives the equivalent. Mix thoroughly, scraping the walls and bottom, using the stated method.

Mount the tumbler firmly. It should rotate without wobble or slip, and the turner and cup should be aligned and level for the shape. Slow, continuous rotation is a common way to spread the coating evenly. [2]

Apply the amount you validated, as a controlled film. Then check the shoulder, the base transition and the decal edges — that’s where excess or thin spots hide. Resist adding more just because the wet surface looks uneven while it settles.

Keep rotating for the time you established for that material and those conditions, then cover the cup against dust while it cures. No one speed or duration suits every resin and cup, so record your own validated settings rather than copying a random tutorial.

Build coverage around the decoration

Fine glitter, coarse glitter, flat vinyl and raised embellishments each demand something different. A design that feels smooth under epoxy on one cup can leave coarse particles sticking out on another.

If you need extra coats, respect the recoat window and the prep the product requires. One heavy layer meant to bury texture tends to creep and pool at the base. Follow the approved coating sequence, and don’t treat the maximum allowed thickness as a target.

Never sand resin that hasn’t reached the right cure state. If cured resin needs leveling, follow the supplier’s abrasion and dust-removal guidance before recoating. And if a surface stays soft or tacky, find out why before covering it with another layer.

Diagnose uneven coverage before changing the formula

Fisheyes. Look at contamination and compatibility first, not viscosity. Oils, residues and some surface treatments stop resin from wetting out. Test your cleaning method on the actual paint or sealer so the fix doesn’t damage it.

Ridges and heavy ends. Check the applied amount, cup alignment, temperature and when rotation stopped.

Rough glitter. Ask whether the particles were locked down, and whether the approved coating build actually covers the texture.

Bubbles. Separate air from mixing from air trapped around decoration. Use the formulation’s approved removal method. Extra heat isn’t a universal cure — it can change flow, speed the cure or damage the decoration beneath.

Sticky streaks. Go back through your measuring and mixing records. If the whole cup cures slowly, review temperature, elapsed time and component pairing. Don’t change the resin-to-hardener ratio to force a faster result.

Qualify your tumbler resin before buying in bulk

Distributors and craft brands should ask for the current technical data sheet and safety data sheet, plus guidance for the intended cup surface. Ask about mixed viscosity, thin-film cure, recoat requirements, storage, packaging and batch identification.

Then run a small trial with your typical decorations and your hardest designs. Hold cup type, application amount, room conditions and turning setup constant while you compare candidates. Log defects and rework as carefully as you log the good-looking samples.

Compare cost per acceptable cup, not cost per kilogram. A cheaper resin gets expensive when it needs more correction, extra coats or longer turner time. Agree measurable acceptance criteria with the supplier before you scale up.

Jinhua Resin lists a tumbler resin for wholesale sourcing. When you request samples, share your cup material, decoration, target process time and packaging needs. Check the selected grade’s own documentation and performance — don’t apply another formulation’s instructions to it. [3]

Full cure and care instructions finish the product

Let the finish reach its specified full cure, under documented conditions, before anything ships. A coating that feels dry can still mark in the box if it hasn’t developed its final properties.

Give customers care instructions for the validated cup. Hand washing with a soft cloth and avoiding abrasive cleaners is the common advice for resin tumblers. Don’t promise dishwasher, microwave, long-soak or high-heat suitability without specific support. [4]

The best epoxy resin for tumblers is the one that gives you consistent coverage in your own process. Match the coating to the decorated surface, control how much you apply, and verify the cure before you run production. Those habits do more for a smooth finish than one more layer applied without knowing what went wrong.
Epoxy Resin Oem

Epoxy Resin OEM & ODM: Quality Control from Sample Development to Bulk Production

Most buyers who run into trouble with epoxy resin OEM orders don’t get burned on price. They get burned on consistency. The sample was crystal clear, the first pallet was fine, and by the third shipment customers are emailing about yellowing, soft spots and bubbles that won’t leave.

That almost never means the factory “made a bad batch.” It means the factory never turned a good sample into a repeatable process.

This guide walks through the full epoxy resin OEM and ODM cycle in the order it actually happens, with the quality checkpoints that matter at each stage. It applies whether you’re sourcing table top epoxy, deep pour epoxy or UV resin.

Epoxy Resin Oem

OEM vs. ODM: Who Owns the Formula?

The two terms get mixed up constantly, and the difference changes how much risk you carry.

OEM means you supply the specification, or sometimes the formula itself, and the factory produces it under your brand. ODM means you describe the result you want, such as “deep pour, 5 cm in a single pour, water-clear, no yellowing,” and the epoxy resin manufacturer develops the formulation.

In practice, most private label epoxy resin projects land somewhere in between. The factory starts from a proven base formula and adjusts it for your market: viscosity, cure speed, color, pot life. It’s faster than a ground-up ODM project, and it carries far less risk than inventing a formula from scratch. If you’re a first-time importer, this hybrid route is usually the smart one.

Step 1: Write a Brief That Leaves No Room for “Close Enough”

Quality disputes in epoxy resin OEM projects usually trace back to a vague brief. “Similar to Brand X” isn’t a specification. A usable brief covers:

  • Product type and application: table top, river table, jewelry casting, floor coating
  • Pour thickness per layer: roughly 2–3 mm for table top, 25–50 mm or more for deep pour
  • Target viscosity at 25°C, in mPa·s
  • Mix ratio, by volume or weight, and working time
  • Demold or full-cure time, and target Shore D hardness
  • Destination market and its compliance needs: REACH, Prop 65, RoHS, TSCA

That last item gets skipped more than any other. A formula built for one market can fail another market’s requirements, and reformulating after you’ve approved samples costs weeks. Settle it before the first sample is mixed.

Step 2: Sample Development Should Test Stability, Not Looks

A reputable epoxy resin manufacturer typically delivers first-round samples within 7–14 days when working from an existing base formula. Don’t judge them by clarity alone. Clear samples are easy. Stable ones are hard.

Pour it the way your customer will. Lab conditions at 25°C tell you little about a customer’s garage at 15°C. Test at realistic temperatures, in realistic molds, at realistic thicknesses. For deep pour epoxy, watch for exotherm: a formula that runs hot in a thick pour can crack, yellow or cure unevenly.

Run an aging comparison. Yellowing is the single most common complaint in the resin trade. Ask the factory for UV aging or accelerated weathering data, or run your own side-by-side: a sample and a control placed in strong light for several weeks, then compared for color shift.

Sign off on a reference sample. Both sides keep a sealed retained sample marked with batch number, date and key parameters. Every bulk shipment gets judged against it. Without that reference sample, any later dispute becomes one side’s word against the other’s.

Step 3: The Pilot Batch That Locks the Formula

Lab samples are measured in grams. Bulk production is measured in tons. Scale-up changes things: heat builds up differently in a large reactor, mixing efficiency shifts, degassing takes longer, and filling lines introduce new contamination risks.

That’s why a serious epoxy resin OEM process includes a pilot run, commonly 100–500 kg, before any full order. The pilot answers three questions:

  1. Do viscosity, color and cure profile at scale match the approved sample?
  2. How much does normal raw material variation move the final result?
  3. Does filling and packaging add moisture, dust or other contaminants?

Once the pilot passes, the formula and process parameters get frozen in a written work instruction. After that, changing a raw material supplier or adjusting a ratio requires written notice to you and re-approval. If a factory resists this, it’s a red flag. Silent substitutions are how consistent products turn inconsistent.

Step 4: Quality Control During Bulk Production

Consistency in bulk production comes from breaking quality into checkpoints and recording every one, on every batch. Here is what a solid control plan looks like:

StageWhat gets checkedTypical method
Incoming raw materialsEpoxy value, amine value, moisture, colorTitration, Karl Fischer, Gardner color
In-processCharging accuracy, mixing time, reaction temperatureWeighing system records, temperature logging
IntermediateViscosity, densityRotational viscometer (ASTM D2196), ASTM D1475
Finished product releaseMix ratio check, gel time, cured hardnessASTM D2471, Shore D (ASTM D2240)
PackagingNet weight, seal integrity, batch labelingSample weighing, visual inspection

Viscosity is the number to watch. A common industry tolerance is about ±10% against the approved value. If gel time drifts well outside the agreed window, something is wrong with the raw materials or the ratio, and that batch shouldn’t ship.

Traceability is non-negotiable. Every drum or kit should carry a batch code that links back to raw material lots, production date, operating team and inspection records. When a customer reports a problem three months after delivery, a capable epoxy resin manufacturer can pull the batch history within hours, not days.

Step 5: Pre-Shipment Inspection and Retained Samples

Before goods leave the factory, you should receive:

  • A certificate of analysis (COA) for each batch, showing measured viscosity, gel time, hardness and other agreed parameters
  • SDS and TDS documents matched to the product, which customs brokers and end customers will both ask for
  • Retained samples, kept by the factory for at least 12 months per batch

Retained samples matter more than most buyers realize. If a customer reports abnormal curing half a year later, you can compare the retained sample against the returned product and settle the question with evidence.

On your first order, do your own incoming check too. Pull random units, mix and pour them by the standard method, and compare against your reference sample. It costs very little, and it exposes problems while you still have leverage.

Questions to Ask Before You Commit to an Epoxy Resin OEM Supplier

You can learn a lot about a factory from how it answers plain questions:

  • Do you run your own lab, and can you share batch-level test data rather than a generic datasheet?
  • How do you notify customers about formula or raw material changes?
  • Is a pilot run part of your development process, or an optional extra?
  • How long do you keep retained samples?
  • Can you provide compliance documents for my target market?
  • Are you a factory or a trading company? (Ask to see the production floor, even by video.)

A true epoxy resin manufacturer won’t be bothered by any of these, because the answers already exist in its daily operations. Vague or defensive replies tell you what you need to know.

FAQ

What is the minimum order quantity for epoxy resin OEM?
It varies by product and packaging. Custom formulas generally carry higher minimums than standard catalog items, since the factory has to dedicate production time and sometimes custom packaging. Ask for MOQs per product line rather than a single number.

How long does it take from sample to first bulk delivery?
When the factory adjusts an existing formula, expect roughly 4–8 weeks including pilot and production. A full ODM development project usually needs 2–3 months, sometimes longer if compliance testing is involved.

Can I sell epoxy resin under my own brand?
Yes. Private label epoxy resin is the core of OEM service: your label, your packaging design, your kit configuration. Confirm artwork lead times early, since packaging often becomes the bottleneck.

How do I avoid batch-to-batch differences in color and viscosity?
Require incoming inspection on raw materials, a locked formula after the pilot run, and a COA with every shipment. Those three controls prevent most drift.

Should I test every shipment myself?
On the first two or three orders, yes. Once the factory has proven consistent, periodic spot checks are usually enough.

Final Word

Good epoxy resin OEM results don’t come from one perfect sample. They come from a process that repeats: a clear brief, a signed reference sample, a pilot batch that locks the formula, and test data that follows every shipment.

If you’re looking for an epoxy resin manufacturer with OEM and ODM capability, tell us your target market and application, and we’ll start with a sample plan built around your specs.

Cold Weather Epoxy Resin

Cold Weather Epoxy Resin: Temperature, Amine Blush and Winter Pouring Fixes

Epoxy doesn’t care what the calendar says, but it cares a lot what the thermometer says. Pour cold weather epoxy resin in a garage at 50°F and you can end up with a surface that stays tacky for days, a greasy film that won’t wipe off, or bubbles frozen in the middle of the pour. None of that means the resin is bad. The room was just too cold for the chemistry.

Winter is when distributors and shops see the most complaints, because customers keep pouring while the heat drops. This guide covers the minimum temperatures that matter, what amine blush is and how to fix it, what to do when resin shows up cold or crystallized, and a checklist you can hand to customers. If you buy from an epoxy resin manufacturer for resale, the last two sections are aimed at you.

Cold Weather Epoxy Resin

How cold is too cold for epoxy?

Most data sheets give a working range of roughly 70–80°F (21–27°C), with a floor around 60°F (16°C). That floor applies to the resin, the hardener, the surface you’re pouring on and the air, not just the number on the wall thermostat. Below it the reaction slows hard. As a rule of thumb, reaction speed roughly halves for every 18°F (10°C) of cooling, so a resin that cures in 24 hours at 77°F can take far longer at 55°F, and at some point it just stops short of a full cure.

Look for the stated minimum on your TDS. If the sheet doesn’t give one, ask the epoxy resin manufacturer, and until you hear back treat 60°F as the line.

What cold does to resin and hardener

Slow cure. Epoxy that should be hard in a day or two stays soft or tacky, sometimes for a week. The surface may feel dry while the layer underneath is still gel.

Thick resin. Cold epoxy is far stiffer, so it levels badly and holds on to bubbles. We cover the mechanics in our guide to epoxy resin viscosity.

Crystallization. After a cold truck ride or a night in an unheated warehouse, some resins turn cloudy, grainy or semi-solid in the container. That’s crystallization, and it’s reversible. Loosen the lid slightly, set the container in a warm water bath at about 120–140°F (50–60°C) and keep water out of it. Stir gently until the resin is fully clear, then let it come back to room temperature before you measure. Don’t microwave it or set it on a direct heat source. Leftover crystals throw off the mix ratio, so use it only when it’s clear.

Amine blush. Different problem, bigger headache. It gets its own section.

Amine blush: the waxy film nobody expects

Amine blush is a waxy, greasy or cloudy film that forms on the surface of curing epoxy. It happens when amine groups in the hardener react with carbon dioxide and moisture in the air before they finish reacting with the resin. Cold, damp conditions make it much more likely, because the cure is slow and the surface sits exposed for longer.

You’ll spot it as a hazy, oily or sticky surface on a pour that’s otherwise hard. A fingernail won’t dent the epoxy underneath, but the top feels slick. Blush dissolves in water, so the fix is simple: wash with warm water and a little dish soap, scrub with a nylon pad, rinse, dry, and sand lightly before recoating. Skip the sanding and the next coat may not bond.

To prevent it, keep the surface at least 5°F (3°C) above the dew point, avoid pouring on very humid days, and keep the room warm through the whole cure, overnight included. One more thing. Don’t heat a closed space with an unvented propane or kerosene heater. Those put carbon dioxide and moisture into the air, which is exactly what blush feeds on. Electric heat is the safer choice.

How to pour epoxy in cold weather

  1. Warm the workspace to at least 70°F (21°C) the day before, and keep it there until the cure is finished.
  2. Bring everything inside for 24 hours: resin, hardener, wood, molds, mixing cups. Lumber from a cold shed carries chill and moisture into the pour.
  3. Check the surface temperature, not just the air. An infrared thermometer is cheap, and a hygrometer tells you whether you’re close to the dew point.
  4. If the containers are still cool, warm them in a water bath to about 77–80°F, lids sealed. Stay under roughly 86°F, since hot resin gels fast.
  5. Measure by the TDS ratio and mix for the full time, scraping the sides and bottom. Cold resin needs it.
  6. Cover the pour loosely to keep dust off and heat steady, and keep the room within range for the entire cure. A thermometer left next to the pour tells you what happened overnight.

Resist the urge to rescue a cold pour with a heat gun or a heat lamp parked close to the surface. Concentrated heat makes hot spots, which can yellow the epoxy or cure the top faster than the layer underneath and leave it wrinkled. A small electric heater across the room, or a heated mat under the work surface, gives gentler and more even warmth.

Troubleshooting: cold-weather problems

SymptomLikely causeFix
Still tacky after the stated cure timeToo cold during cure, or off-ratio mixMove it to a room at 70–77°F and give it extra days. If it stays soft after several warm days, the ratio was probably off and the soft layer has to be removed.
Greasy or hazy film on a hard pourAmine blushWash with warm soapy water, rinse, dry and sand before recoating.
Bubbles frozen in the pourCold, thick resinWarm both components, pour in thinner layers, and use a heat gun or torch on thin coats.
Cloudy or grainy resin in the containerCrystallizationWarm water bath, stir until clear, cool to room temperature before mixing.
White haze on the cured surfaceMoisture from damp wood or humid airDry and warm the wood and the workspace before the next pour.

Winter storage and shipping for distributors

If you hold stock, keep it above about 60°F (16°C) all year. A cold warehouse is how crystallized resin and thick, hard-to-pour epoxy end up in your support inbox. Move pallets indoors before a cold snap, let them settle to room temperature before anyone opens a container, and rotate older stock out first. Our guide to shelf life and reorder planning covers the inventory side.

Winter freight adds its own risk. A container that sits in an unheated truck or a port yard for a week can arrive cold, so ask your epoxy resin manufacturer how the product is packed and whether it has temperature recommendations for transit. Tell your own customers the same thing in writing. A short winter note in the order confirmation (store resin indoors, pour at 70°F or above, let containers acclimate for a day) can head off many of these tickets.

Specifying epoxy for cold climates

Not every formula behaves the same at low temperature, and your customers in Minnesota, Ontario or the north of the UK aren’t pouring in the same shop as customers in Arizona. If you sell private label epoxy into a cold market, tell your epoxy resin manufacturer the lowest temperature your customers really pour at, and ask what the formula does there. Our piece on custom-formulated versus standard private label epoxy explains how that conversation usually goes.

Jinhua Resin is an epoxy resin manufacturer making table top epoxy, deep pour epoxy and UV resin under OEM and private label programs. Send us your target climate and your application, and we’ll talk through options.

FAQ

Can you pour epoxy in cold weather?

Yes, as long as the resin, hardener, surface and room all stay inside the range on the TDS, usually about 70–80°F (21–27°C). Once you drop below roughly 60°F (16°C), expect slow cure, thick resin and surface problems.

What temperature is too cold for epoxy to cure?

Cure slows sharply below about 60°F (16°C). Near 50°F (10°C), many epoxies stay tacky or never reach a full cure. Your data sheet gives the real minimum for your product.

How do I get rid of amine blush?

Wash the surface with warm water and a little dish soap, scrub with a nylon pad, rinse and let it dry. Then sand lightly before you recoat. Blush is water-soluble, so solvents aren’t needed.

Is cloudy epoxy resin in the bottle ruined?

Usually not. Cloudy, grainy or semi-solid resin is typically crystallized, and it can be reversed. Warm the container in a water bath until it’s clear, then let it cool to room temperature before mixing.

Does a heat gun help epoxy cure in cold weather?

A heat gun helps pop surface bubbles on thin coats, but it won’t cure a pour. Steady, even warmth in the room does that. Keep the heat gun moving so it doesn’t scorch the surface.

Epoxy Resin Yellowing Test

Epoxy Resin Yellowing Test: How to Verify Anti-Yellowing Performance (UV Aging, Color Difference and Light Transmittance)

Ask a supplier whether their clear epoxy will yellow, and the usual answer is “we added UV stabilizers.” That proves nothing.

Yellowing resistance is measurable. The sample prep, the aging protocol and the way you read the numbers all follow established methods. Here is how an epoxy resin yellowing test works in a lab, step by step.

Epoxy Resin Yellowing Test

Where Yellowing Comes From

Two mechanisms cause it, and they need different tests.

Photo-oxidation. UV light breaks polymer bonds and oxidizes the nitrogen in amine hardeners, which creates color-forming groups. This is the main cause for anything near a window or outdoors. UV aging tests target it.

Thermal oxidation. Heat alone can discolor the hardener, no sunlight needed. A resin sitting under a hot lamp or in a heated enclosure can turn amber anyway.

A UV test by itself leaves half the picture blank. If the product will see heat, run a thermal aging group alongside it.

Sample Preparation: Where Most Bad Data Starts

Most unreliable results come from the samples, not the equipment.

  • Match the thickness. Cast clear plaques at 3 mm (about 1/8 inch) and keep every sample in the comparison identical. A 1 mm difference shifts both transmittance and b* values enough to wreck the comparison.
  • Cure fully. Let samples cure at room temperature for at least 7 days. Post-cure reactions during testing will contaminate the data.
  • Keep a control. Store one plaque from each batch in the dark. Every color shift is calculated against it.
  • Use the same mold surface. Different release surfaces give different finishes, and surface finish changes haze readings.
  • Weigh, don’t measure by volume. Mix by weight on a scale. Measuring cups introduce ratio errors that show up as color drift.

UV Aging Setup

The standard tool is a fluorescent UV chamber (QUV), run under ASTM G154 or ISO 4892-3.

Typical settings:

  • Lamps: UVA-340, which best matches the short-wave UV portion of sunlight
  • Irradiance: 0.89 W/m² at 340 nm
  • Cycle: 8 hours UV at 60°C (140°F), then 4 hours condensation at 50°C (122°F)
  • Check points: 0, 250, 500 and 1,000 hours

For outdoor or high-transparency applications, add a xenon arc run under ISO 11341. The spectrum is broader, though the cost and test time go up.

One caution when you talk to customers: chamber hours don’t convert cleanly into years outdoors. Solar exposure varies too much by region. Treat the hours as comparison data between formulations, never as a lifespan guarantee.

Color Difference: Three Numbers That Matter

At each check point, measure L*, a* and b* with a spectrophotometer, then calculate ΔE following ASTM D2244. Yellowing shows up mainly in b*, since a rising b* means the sample is moving toward yellow. You can also calculate the Yellowness Index (YI) under ASTM E313.

MetricWhat it tells youRule of thumb
Δb*Shift along the yellow–blue axisAbove 1, visible in side-by-side comparison
ΔETotal color changeUnder 1 is effectively invisible; 1–3 needs a reference to notice; above 3 is obvious
YIYellowness indexLook at the increase, not the absolute value

A reasonable internal benchmark for tabletop and deep pour epoxy is ΔE under 3 and Δb* under 2 after 500 hours. That is a common in-house approach, not an industry-wide standard, so adjust it to the product’s positioning.

Light Transmittance and Haze

Yellowing is only part of aging. Degraded resin often develops micro-cracking or surface bloom, and clarity drops with it.

Measure transmittance and haze with a haze meter under ASTM D1003. A good clear epoxy at 3 mm typically sits around 90% transmittance when fresh. What matters is the change after aging: how many points transmittance falls and how far haze climbs.

This catches a failure mode color data misses. A sample can show a small ΔE and still have rising haze, which means the surface has started to break down.

Traps When Reading a Test Report

A single data point. A report with only the 1,000-hour result hides the trend. Some resins hold steady early and collapse late; others drift from hour one. The curve says more than the endpoint.

Missing thickness or color. Thin plaques always look better than thick castings. Data without thickness isn’t comparable.

Cross-system comparisons. Table top epoxy, deep pour epoxy and UV resin use different chemistry. Comparing their yellowing numbers against each other tells you nothing. Compare within the same product type.

No dark-stored control. Without one, you can’t separate aging-induced yellowing from a resin that started slightly yellow.

What Buyers Should Ask For

When you request a report from an epoxy resin manufacturer, ask for five things: the test standard, the lamp type, the irradiance, the sample thickness and the raw readings at each interval. A supplier that hands all five over without hesitation is probably running a disciplined process. One that can’t produce them is likely selling a marketing claim.

If you can, request samples and run your own side-by-side. Same chamber, same batch of plaques, same check points. Nothing is more convincing than data you generated yourself.

No formulation is yellow-proof forever. The light stabilizer package, the hardener system and the real-world environment all play a part. The only reliable way to know how a resin performs is to test it.

Epoxy Resin Customer Complaints

How to Handle Epoxy Resin Customer Complaints: A Troubleshooting Workflow for Distributors

A customer emails a photo of a sticky tabletop and asks for a refund. Another says the resin went solid in the mixing cup before a drop reached the mold. Both call the product defective. Neither photo tells you why.

That gap is the whole problem. Handling epoxy resin customer complaints well means running the same process every time: stop the loss, collect evidence you can compare, check it against the right instructions, and agree on a remedy in writing. Do that, and you protect the customer — and give your epoxy resin manufacturer enough detail to spot a genuine material fault.

A scope note first. This workflow fits two-component epoxy used for crafts, tabletops and casting. Floor coating complaints can share the same record, but they also need substrate testing and a site assessment. UV resin is a different animal. It cures under light, so investigate it separately and never judge it by epoxy mixing rules.

Epoxy Resin Customer Complaints

Step 1: Acknowledge quickly, then contain the loss

Start with the practical damage. The customer may have lost a finished piece, missed a delivery or stopped a production line. Give them one contact person, open a case number and say when the next update will arrive. A dated promise to update beats a rushed promise to confirm the cause.

Ask the customer to stop using the affected kit and keep the containers, labels and leftover components. Photograph everything before anyone tries a repair. If the report points to a possible batch problem, identify the stock involved and put it on temporary hold while technical staff review.

One exception overrides routine troubleshooting. If material is overheating, smoking or leaking, safety comes first. Send the customer to the product safety instructions and the right emergency response. Never tell anyone to pick up a hot container or improvise a chemical cleanup.

Keep your first message neutral: “We will review the batch and the application conditions together.” A photo alone justifies neither admitting a manufacturing defect nor blaming technique.

Step 2: Build one complete complaint record

A solid epoxy resin troubleshooting workflow runs on facts you can line up side by side. Ask for them in a single form or message. Drip-feeding a new question every day wears out the customer and stalls the case.

The record needs five blocks:

  • Product: exact name and grade, order number, purchase date, and the batch numbers on both resin and hardener. Different batch numbers do not by themselves prove a wrong pairing.
  • Mixing: amounts actually dispensed, whether by weight or by volume, tools used, mixing method, and any transfer to a second container. A ratio quoted without its measuring basis is incomplete.
  • Conditions: material temperature, room and substrate temperature where relevant, rough humidity, batch size, cup dimensions, applied thickness, and how long after mixing the defect showed up.
  • Additives and history: pigments, inks, fillers, solvents, release agents, sealers, earlier coatings, plus storage and transport conditions. Quantities where known.
  • Evidence: a wide shot, close-ups, label photos and a timeline from mixing to inspection. Keep observations apart from estimates. “Temperature not recorded” is better evidence than an invented room-temperature figure.

Step 3: Describe the symptom before you argue about the cause

“Bad resin” is not a symptom. Turn it into something specific. Is the whole casting soft, or only a few sticky streaks? Did the material gel in the cup, or did a deep casting crack days later? Did the coating lift off the wood, or did the wood itself split?

Note when and where it happened. A defect along one edge points somewhere different from one that appears in every piece. Ask whether other kits or runs were affected — and whether any run under similar conditions came out fine.

Keep three fields separate in the case file: observed symptom, possible explanation, confirmed finding. “Customer reports tacky patches” is an observation. “Incomplete mixing may be involved” is a hypothesis. Only records or testing can move a hypothesis toward a conclusion.

Step 4: Check the instructions for the exact epoxy system

Pull the technical data sheet and label instructions that shipped with the order, including the right revision. Confirm the measuring basis, application limits and cure conditions. A table top formula and a deep pour formula do not share a processing window, so never assume they do.

For slow or incomplete cure, compare the real resin and hardener amounts with the specified ratio. Weight and volume ratios are not automatically interchangeable. Then ask which milestone the customer inspected — demolding, handling or full cure. They are three different points in time.

One rule has no exceptions: do not tell anyone to add extra hardener to speed things up, or to brush hardener over a tacky surface. An unmeasured addition after application cannot fix a wrong ratio. The right response depends on whether you face delayed cure, incomplete mixing or a material that cannot cure properly.

For fast gelation, look at temperature and how much mixed material stayed in the container. Mixed epoxy builds heat, and the safe limits depend on formulation and geometry. If you run a reproduction trial, use the supplier’s approved batch size and thickness.

Step 5: Work through the symptom checklist

SymptomWhere to look first
Soft or stickyComponent identity, measuring basis, mixing completeness, temperature, additives, time allowed to cure. Localized streaks versus uniform softness is a useful clue, but never proof by itself.
BubblesDid air arrive during mixing, rise from a porous substrate, or appear as the material warmed? Ask for photos of the substrate and any seal coat. Do not prescribe a torch or extra heat before checking the product instructions.
Fisheyes or cratersSurface cleaning and contamination from oils, silicone products, tools or earlier treatments. Contamination is a recognized lead, yet the exact source still needs investigating.
PeelingWhich interface failed: epoxy to substrate, one layer to another, or inside the underlying material? Record preparation, moisture and recoat timing. A detached sample often says more than a photo.
Yellowing or cloudinessDid the look change before mixing, during cure or after service exposure? Compare like-for-like samples under the same lighting. Not every color shift has the same cause.

Step 6: Run controlled comparisons with the manufacturer

Escalate with a tight evidence package, not a forwarded chat thread. Include the case summary, product and batch details, photos, processing records, suspected causes and the outcome the customer wants. List what is still missing.

Where it makes sense, ask the manufacturer to compare a retained sample against material from the complaint. A good plan has three parts: an unmodified sample processed to specification, a known acceptable reference, and a separate trial that reproduces the reported conditions. Change one variable at a time, or the results mean nothing.

Log sample identity, quantities, container shape, temperatures, additives and observations at agreed intervals. Set acceptance criteria before testing starts. “Looks fine” won’t do when the complaint is about surface tack or adhesion.

Read the results with care. A retained sample that passes does not wipe out the complaint — storage, transport, packaging or that one kit may still be at fault. A failed customer sample does not put the blame on the factory either, not without knowing how it was handled. State what each comparison can and cannot show.

Step 7: Agree on a proportionate resolution

The technical finding and the commercial remedy are linked, but they are separate decisions. Depending on the evidence and your terms, the answer could be replacement material, a credit, a refund, application guidance or a jointly reviewed repair plan.

If a material issue is supported, record the affected scope and explain how replacement stock will be checked. If an application factor is supported, show the evidence politely and name the process change. If the cause is still unclear, say so. Record any goodwill gesture as goodwill, not as a proven technical conclusion.

Never promise that a fresh coat fixes every sticky surface or that warming will rescue every failed casting. Some jobs need removal and a rebuild. Others just need more time under specified conditions. Get a product-specific repair recommendation before asking the customer to spend more material or labor.

For site conditions, structural performance or serious property damage, remote advice is not enough. Arrange a proper technical assessment before anyone recommends irreversible work.

Step 8: Close the case and stop it from coming back

Close only after you have recorded the agreed action and checked that it worked. Keep the final finding, the evidence reviewed, the remedy, the person responsible and any preventive action. Ask the customer whether the replacement or revised process actually solved the problem.

Correction and prevention are different jobs. Replacing a kit fixes today’s loss. Rewording a confusing ratio label may prevent next month’s complaint. Other options: clearer dispensing instructions, better storage guidance, an approved colorant list, or extra checks when components are packed.

Track patterns with proper denominators. Five reports mean one thing across fifty kits and another across fifty thousand. Compare rates by product, batch, application and shipment period, and allow for how customers use the product. Several independent reports on one batch should trigger a review before the root cause is confirmed.

Useful service measures: time to first response, time to an agreed next action, repeat complaint rate and completion of preventive actions. Speed matters. But a case closed fast is not necessarily a case solved.

A worked example

A customer reports sticky areas on a countertop. The distributor pauses further coating and collects labels, ratio records, photos and the mixing timeline. The images show isolated streaks, while another section from the same kit has cured firm.

The distributor doesn’t declare a defective batch, and doesn’t blame the customer either. It asks how the material was scraped and transferred. The manufacturer then proposes controlled comparisons with correct proportions and documented mixing. Suppose the reference trial performs as specified, while a trial that mimics incomplete mixing reproduces the streaks.

That supports a mixing-related explanation under the tested conditions. It does not prove every sticky countertop has the same cause. The distributor logs the evidence, gets a repair recommendation, agrees a commercial response and improves the mixing guidance in future orders.

FAQ

Should distributors replace every complained-about kit immediately?

Sometimes replacement is a sound commercial call. It should not end the investigation. Keep the batch information and the leftover material, or repeated replacements will hide a recurring problem.

Can photos prove an epoxy resin is defective?

They document appearance and location. They usually cannot establish the original ratio, internal cure, storage history or responsibility without more evidence.

When should the manufacturer get involved?

Escalate promptly for repeated reports, suspected batch inconsistency, safety concerns or anything beyond your technical reach. Send the facts you have and say clearly what remains unknown.

A dependable epoxy resin customer service process gives both sides a clear next step. If you source from Jinhua Resin or another epoxy resin manufacturer, start with a traceable case record and a product-specific technical conversation. That is how you get fair remedies, clearer instructions and fewer repeat complaints.

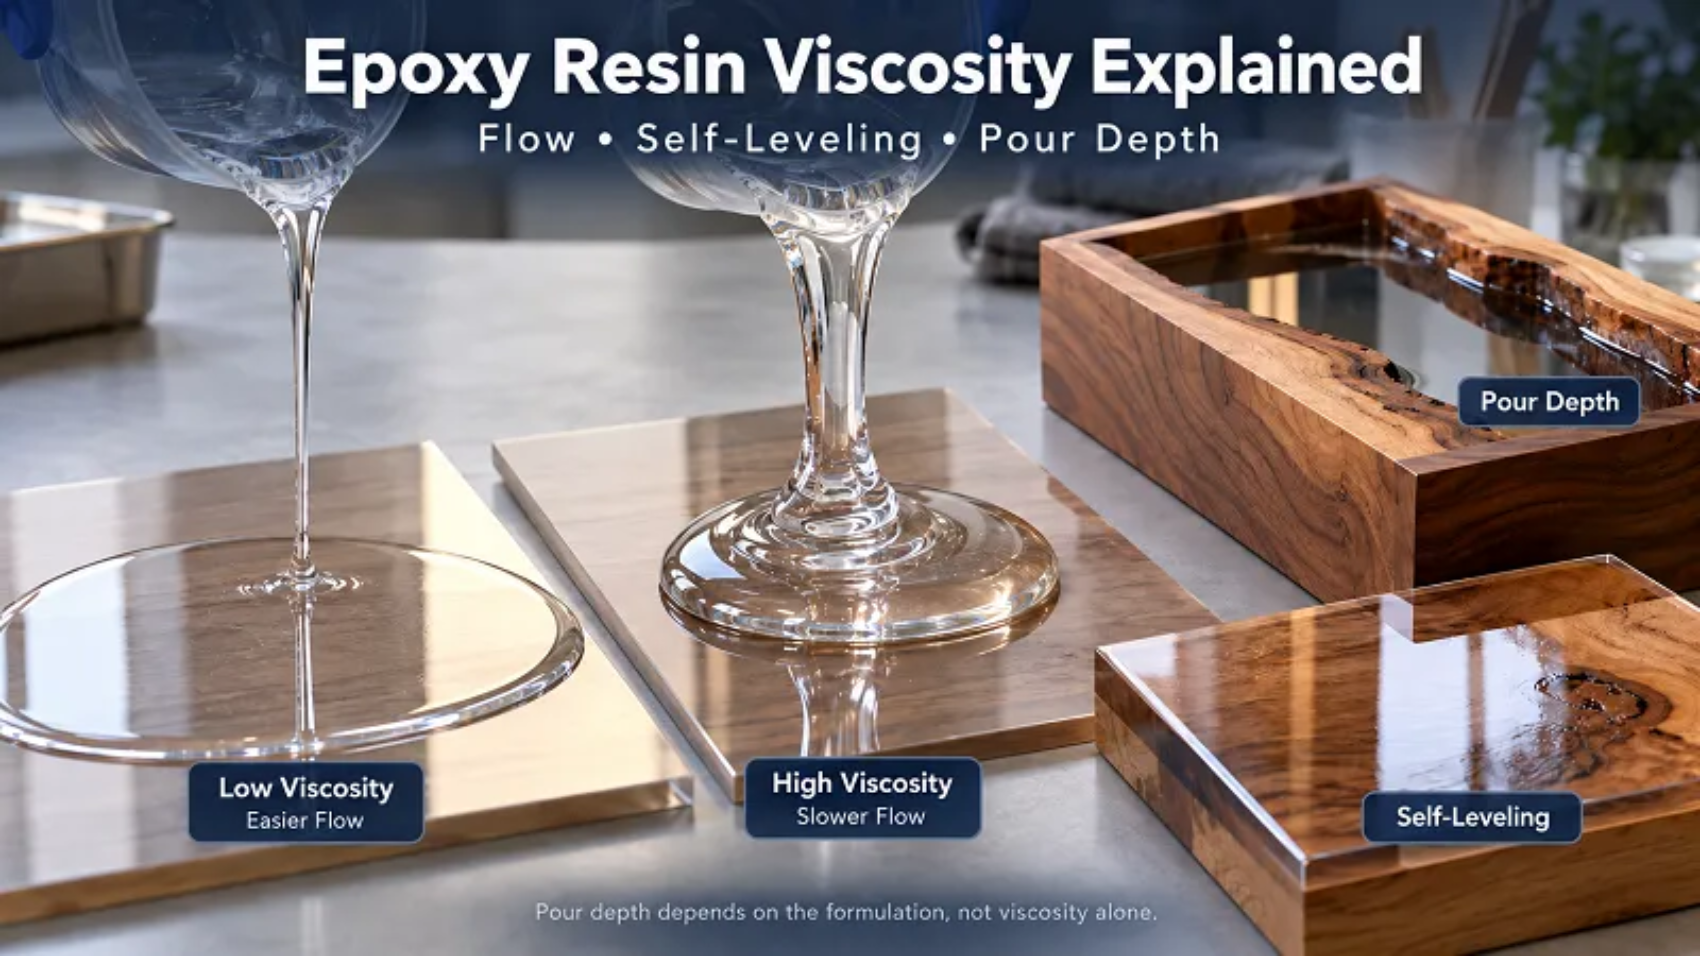
Epoxy Resin Viscosity

Epoxy Resin Viscosity Explained: How Thickness Affects Flow, Self-Leveling and Pour Depth

Price, clarity, cure time. That’s what most buyers compare when they line up two epoxies. Viscosity gets skipped, and it shouldn’t, because it controls things you actually see on the job: whether a flood coat flattens out or leaves ridges, whether bubbles reach the surface of a deep pour, whether the resin sits on the edge of a table or ends up on the floor.

Get it wrong and it comes back as a return. Someone grabs a thin casting resin to coat a bar top, or a thick coating resin to fill a river table, and the review says the epoxy is bad. The epoxy was fine. It was the wrong epoxy.

Below: what epoxy resin viscosity is, how it’s measured, what pushes it up and down, and how to match it to a job. If you buy from an epoxy resin manufacturer for resale or private label, the last two sections are for you.

Epoxy Resin Viscosity

What epoxy resin viscosity actually means

Viscosity is how hard a liquid resists flowing. Water is about 1 cP (centipoise). Olive oil is near 80. Honey runs anywhere from 2,000 to 10,000 depending on the kind and how warm it is. Most pourable epoxy lands somewhere between thin syrup and runny honey.

A few things trip people up on data sheets. cP and mPa·s are the same unit, so 1,000 cP is 1,000 mPa·s, no conversion needed. Temperature matters more than the number itself: a viscosity figure only means something next to the temperature it was tested at, usually 77°F (25°C). A resin listed at 560 cP at 86°F (30°C) isn’t thinner than one listed at 800 cP at 77°F. They could be nearly the same product.

And there isn’t just one viscosity. Part A, Part B and the mixed resin each have their own, with A usually the thicker side. The mixed figure is what you pour, and it keeps climbing while you work.

Typical viscosity by product type

These ranges are typical for the industry and meant for orientation only. For a specific product, trust the TDS from your epoxy resin manufacturer over any chart, this one included.

Product typeTypical mixed viscosity (at 77°F / 25°C)Typical thickness per pourWhy it is built that way
Seal coat / penetrating epoxyUnder about 500 cPVery thin coatSoaks into wood grain and seals pores before the main pour.
Deep pour / casting epoxyRoughly 300–1,000 cPUp to about 2 in (5 cm) per layerThin enough for bubbles to rise out of a thick pour before it gels.
Table top / flood coat epoxyRoughly 1,000–3,000 cPAbout 1/8–1/4 in (3–6 mm)Holds on the edges and levels without running away.

What changes epoxy resin viscosity

Temperature is the big one. Warm epoxy flows, cold epoxy doesn’t. As a rough guide, viscosity can drop by about half for every 18°F (10°C) you warm it, though every formula has its own curve. A resin reading 1,200 cP at 77°F might be nearer 800–900 cP at 86°F (30°C). You pay for that with working time, since warm resin reacts faster and gels sooner. Most people keep both containers somewhere in the 77–86°F range; check your TDS. Storage counts too. Resin that spent the night in a cold warehouse pours much thicker than the data sheet says, so give containers a day to come up to room temperature, especially in winter when shipments tend to arrive cold.

Time works against you from the second you mix. Viscosity creeps up slowly at first, then speeds up as the resin heads for gel. A pour that levels like glass at minute 10 can show ridges at minute 40. The resin hasn’t gone bad. It’s just too thick to move.

Fillers and colorants thicken the mix. Mica, pigment paste, glow powder and silica all do it, and a heavy load can leave resin stiff and slow to degas. Our guide to table top epoxy pigments has safe loading limits.

Formulation is the part buyers can’t see. Reactive diluents thin the resin and then bond into the polymer, which is fine in moderation and costs you hardness and chemical resistance if overdone. Some cheap products use non-reactive solvents instead, and those can bring shrinkage, haze and a soft cure. Ask your epoxy resin manufacturer what’s in the bottle.

Viscosity and self-leveling

Flow drives self-leveling, and viscosity drives flow, up to a point. Thinner resin spreads and levels faster. Go too thin and it runs off the edges, leaves corners bare and soaks into porous wood before it cures. Thicker resin stays put and builds a more forgiving coat, but it levels slowly, holds bubbles and can show tool marks if it gels before it settles.

Table top epoxy lives in the middle on purpose. It flows out across a surface, yet it’s thick enough to hold a 1/8-inch coat on an edge until it gels. Three things are in your hands on a flood coat: room and resin temperature (roughly 72–80°F / 22–27°C), pour thickness, and how long you wait between mixing and spreading. Sort those out and a mid-range resin does most of the work.

Viscosity and bubbles

Bubbles climb at a speed set by viscosity. Thin resin lets them go quickly. In a 1/8-inch table top coat they only have a few millimeters to travel, so one pass with a heat gun or torch clears them. In a 2-inch pour the trip is much longer, and resin that’s too thick or too cold cures with bubbles stuck halfway up.

If bubbles are the complaint, look at temperature before anything else. Cold resin traps more air than a bad batch ever does. Technique counts, too. Stir slowly, scrape the sides and bottom of the cup, and don’t whip it, because thick resin won’t give back the air you beat in.

Viscosity and pour depth: a common mix-up

This one gets confused a lot. Low viscosity doesn’t buy you extra pour depth. Depth is capped by exotherm, the heat the reaction gives off. In a thick pour that heat has nowhere to go, and an overheated pour can yellow, crack or shrink. Deep pour epoxy gets its depth rating from a slower hardener that lets heat out gradually. It’s also made thin so bubbles escape before gel. Two separate design choices that happen to show up together.

So don’t pour table top epoxy deep just because it flows nicely. Read the maximum pour depth on the TDS, not the cP number. A reputable epoxy resin manufacturer rates depth from exotherm testing, not from how thin the resin looks in the pail.

Seal coats, wood and edges

Wood holds a lot of air. Pour thick resin over raw wood and that air comes up through the resin during cure, leaving craters and pinholes. A thin, low-viscosity seal coat soaks into the grain first and gives the air a way out before the real pour. For live-edge slabs and river tables, a seal coat followed by a deep pour formula is the usual route. Open edges on a bar top need tape or a dam before you flood.

Troubleshooting: when viscosity is the culprit

SymptomLikely viscosity causeFix
Resin runs off the edges, thin at cornersToo thin for a flood coat, or resin too warmSwitch to a table top (thicker) formula, tape or dam the edges, and let overheated resin cool toward room temperature.
Ridges, brush marks or orange-peel textureResin too thick or too cold; spread too lateWarm the resin to about 77–80°F and get it spread earlier in the working time.
Bubbles trapped in a deep pourResin too thick or too coldWarm both components, use a deep pour formula and pour in thinner layers.
Dull or dry spots over woodThin resin soaked into a porous surfaceSeal the wood first, then do the main pour.
Streaks or clumps after adding powdersFiller load pushed viscosity past what mixing can handlePre-wet the powder in a little resin and cut the loading.

How to read viscosity on a TDS

If you’re buying for resale, check four things on the data sheet. Is the figure for the mixed resin, or just Part A and Part B? What temperature was it tested at? (77°F / 25°C is the common standard.) How was it measured? Viscometer type, spindle and speed all change the reading, and two labs can disagree on the same resin. And what pot life and maximum pour depth are printed next to it?

Even with all that matched, two resins at the same cP can behave differently, because reactivity and flow behavior vary by formula. Ask the epoxy resin manufacturer for a sample and pour it at your own temperature before you commit to volume.

Specifying viscosity for OEM and private label

Viscosity is one of the first numbers to settle on a private label project. Tell the factory the application (flood coat, deep pour, seal coat), the pour thickness you want, and the temperatures your customers really work in. Arizona and Minnesota need different resins. A formula that levels beautifully at 85°F can be too stiff at 60°F.

Jinhua Resin is an epoxy resin manufacturer making table top epoxy, deep pour epoxy and UV resin under OEM and private label programs. Send us your application and a target viscosity range, and we’ll talk through a formula to match.

FAQ

What is a good viscosity for epoxy resin?

It depends on the job. Deep pour and casting epoxies usually run roughly 300–1,000 cP, while table top and flood coat epoxies sit around 1,000–3,000 cP at 77°F (25°C). Match the product to the application and check its TDS.

Is lower viscosity epoxy better?

Not always. Thin resin releases bubbles faster and soaks into wood, but it can run off the edges. Thicker resin holds a heavier coat and levels more slowly.

How do I make epoxy thinner?

Warm the containers gently, to about 77–86°F (25–30°C), before mixing. Don’t thin it with alcohol, acetone or any other solvent. They weaken the cure and can leave haze.

Does viscosity affect cure time?

Not directly. Hardener reactivity and temperature set the cure time. Warm resin is both thinner and faster to cure, which is why people mix the two up.

What does cP mean?

cP stands for centipoise, a unit of viscosity. It is identical to mPa·s (millipascal-second).

Hard Vs Soft Uv Resin

Hard vs Soft UV Resin: Which Type Fits Your Project?

Two resin charms can look identical on the bench. Press one and it holds its shape. Press the other and it bends, then springs back. For a jewelry maker, that’s the whole feel of the finished piece. For a craft brand or distributor, it’s the gap between a satisfied customer and a return.

So how do you settle hard vs soft UV resin? Start with the finished object. If the piece needs a rigid body and a crisp outline, pick a hard grade. If flex is part of the design, look at a soft grade. Then test the formulation with your own lamp, mold, colorants and real part thickness. A label on the bottle won’t do that for you.

This guide covers what separates the two types, where each one fits, and what business buyers should check before a bulk order.

Hard Vs Soft Uv Resin

What Hard and Soft UV Resin Mean

Most craft UV resins are single-component materials that cure under a compatible light source. That sets them apart from the two-part epoxy systems used for river tables and thick castings. Don’t call a UV resin “epoxy” unless your supplier has confirmed the chemistry.

“Hard” and “soft” describe how the resin behaves after proper curing. Hard grades set up fairly rigid. Soft grades stay flexible. Neither word is a standard, though. One supplier’s soft grade may bend far more than another’s, so judge by a sample, not by the name.

One common mix-up: viscosity is not flexibility. A thin, easy-pouring resin can cure rock hard, and a thick, syrupy one can cure bendy. Ask your supplier about the two properties separately.

Hard UV Resin for Pieces That Hold Their Shape

Hard UV resin is the natural starting point for small castings with a defined edge: a flat pendant, a faceted charm, a little ornament. If the design only works when the object stays stiff in the hand, go hard.

That said, hard doesn’t mean scratch-proof or unbreakable. Thin corners, holes drilled near an edge and narrow connection points are all weak spots. A pendant can be fine across its body and still crack at the hole. Test the actual design, not a thick test disk.

If you make batches, run your finishing steps on fully cured samples. Drilling, sanding and fitting hardware put stress on the piece that a freshly demolded casting never sees. Check the area around the fixing point, especially if customers will pull or twist the item.

Soft UV Resin for Designs That Need Flexibility

Soft UV resin suits thin decorative elements and coatings where bending is intended. Think of a flexible petal, a shaped accessory, or a coating on a bendable base. Some commercial soft grades are specifically described as staying bendable after cure.

Flexibility says nothing about adhesion, though. A coating can bend without cracking and still peel off its substrate. Phone-case decoration is the classic example: run the adhesion trial on the exact case material and surface finish. A pass on one plastic doesn’t carry over to another.

Check recovery too. After bending, does the part return to shape, keep a crease, or slowly sag under its own weight? These are good acceptance questions for a trial, but not every soft resin behaves the same way. A long thin strip and a compact charm can respond differently even when poured from the same bottle.

Hard vs Soft UV Resin: Comparing Them Against the Design

Treat this table as a starting point for choosing. It lists priorities, not guaranteed specs.

Selection pointHard UV resinSoft UV resin
Intended cured behaviorRelatively rigidFlexible, to a grade-specific degree
Design priorityShape retentionControlled bending
Trial focusEdges and fixing pointsRecovery and deformation
For coatingsVerify substrate compatibilityVerify both bending and adhesion
For either typeConfirm curing in the actual designConfirm curing in the actual design

Keychains show why an application name alone doesn’t decide it. A small rigid charm leans hard. A flexible decorative insert is worth testing in a soft grade. Both still need solid hardware and a cure that reaches every area. The “best resin for keychains” depends on how the piece is built.

Soft Resin Is Not the Same as Undercured Resin

A flexible result is only expected when you chose a flexible formulation. If a hard resin comes out bendy, leaks liquid or has weak patches, look at your curing process before blaming the grade.

Surface feel can’t prove full cure. A piece may feel firm outside while a shaded pocket inside never got enough light. On the flip side, an intended soft grade shouldn’t be written off just because it bends. Compare it with the supplier’s spec and with a correctly processed reference sample.

For a repeatable check, cure two samples at the same thickness: one uncolored, one with your planned decoration. Follow the supplier’s exposure instructions and let both cool before you judge them. If only the decorated piece fails, suspect light access or additive compatibility. If both are inconsistent, look at the lamp setup and processing conditions.

Light Access Matters for Both Grades

Picking hard or soft doesn’t remove the need for a proper curing setup. Confirm the recommended wavelength, exposure conditions and layer thickness. Lamp wattage alone won’t tell you how much usable light reaches every part of the piece.

Pigments, dense glitter, opaque inserts, mold walls and part geometry all block light. A clear top face doesn’t prove the underside, or the area behind a metal decoration, was cured. Use supplier-approved materials and validate the full design. Manufacturer guidance also notes that adding colorant can lengthen the exposure a given formulation needs.

So don’t turn “cures in one minute” into a production rule. That number may only hold for a clear, thin sample under one lamp. For colored designs or different molds, build a validated process of your own.

How Craft Brands Can Build a Useful Product Range

If you’re a distributor or private-label brand, hard and soft UV resin should answer different customer needs. Two near-identical bottles with vague descriptions just make selection harder and flood your support inbox.

Say plainly what each product does. A hard grade fits rigid decorative pieces. A soft grade fits designs that need verified flexibility. List the compatible lamp requirements and application limits. A photo of a cured sample being bent works well, as long as it comes from the formulation you actually ship.

Look at what your customers already ask. If they want stable pendants, a flexible product won’t solve that. If they decorate bendable objects, a soft grade may be worth exploring, after adhesion testing. Build the range around proven uses, not around every grade on the supplier’s list.

Keep claims tight. “Flexible after curing” is useful. “Never cracks” is a promise you can’t back. Transparency, yellowing resistance and surface durability each need their own evidence. The words “hard” and “soft” don’t prove any of them.

What to Validate Before Ordering Bulk UV Resin

Write a short acceptance brief before you request samples. Cover the part geometry, target thickness, substrate, colorant, lamp, and the movement the product will see in use. Add photos or a sample part if you can. That gives the supplier far more to work with than “send me your best resin.”

Keep conditions identical across candidates. Useful checks include appearance after cure, shape retention, bending recovery where relevant, surface feel, attachment security and adhesion to your chosen substrate. Test at the highest colorant loading you plan to sell, not just on a clear piece.

Define what “pass” means before testing. For example, your team might require a flexible decoration to survive a set bending sequence with no visible cracks or peeling. That’s an internal test method, not an industry certification. Design the sequence around real use and agree it with the supplier if it becomes part of your purchase acceptance.

Read the technical data sheet and safety data sheet for the exact grade. Ask how batches are identified and whether the supplier keeps a reference sample for repeat-order checks. Once a sample passes, document the process. A piece someone remembers looking good isn’t a baseline.

Choosing UV Resin from Jinhua Resin

Jinhua Resin lists a UV resin and a soft-type UV resin for craft applications. You can use the two as a starting pair for comparing a rigid finish with a flexible one. Confirm the exact grade and its current documentation with us before you commit.

When you request a quote, tell us what you make and how you cure it. Include your target bottle size or bulk quantity, your market, and the acceptance checks your business cares about. Ask for a sample that matches your application. Don’t assume any clear UV resin will behave the same.

Jewelry studios usually care most about consistent results in a small mold. Distributors need clear positioning and reliable instructions. A brand developing a flexible decoration may live or die on substrate adhesion and repeated bending. The more of this you share, the easier it is to match a formulation to your product.

Frequently Asked Questions

Is soft UV resin supposed to stay flexible?
Yes, when flexibility is part of the formulation’s design. Confirm the expected degree of movement with the supplier. If a hard grade turns out unexpectedly soft, that’s a curing problem to investigate separately.

Is hard UV resin always more durable?
No. Durability depends on the type of stress, the part geometry, cure quality and the formulation. A rigid piece suits shape retention, while a flexible design may need a softer material.

Can I mix hard and soft UV resin together?
Don’t assume the result will be a predictable middle grade. Use a supplier-approved blend, or ask for a formulation with the properties you want, then validate its cure and performance.

Can soft UV resin be used for thick castings?
“Soft” doesn’t tell you a safe casting depth. Follow the thickness limits in the grade’s documentation. For large or deep pieces, ask whether a different casting system fits better.

Which grade should I buy for a new craft product?
Start from how the finished object has to behave. Decide whether you need rigidity or flexibility, then test the resin with your real production materials before you scale up.

If your design needs a stable shape, hard UV resin is the practical pick. If it needs controlled movement, give soft UV resin a serious look. Either way, pair the choice with a documented curing trial, so the resin performs in your finished product as well as it did in the sample bottle.

Table Top Epoxy Pigments

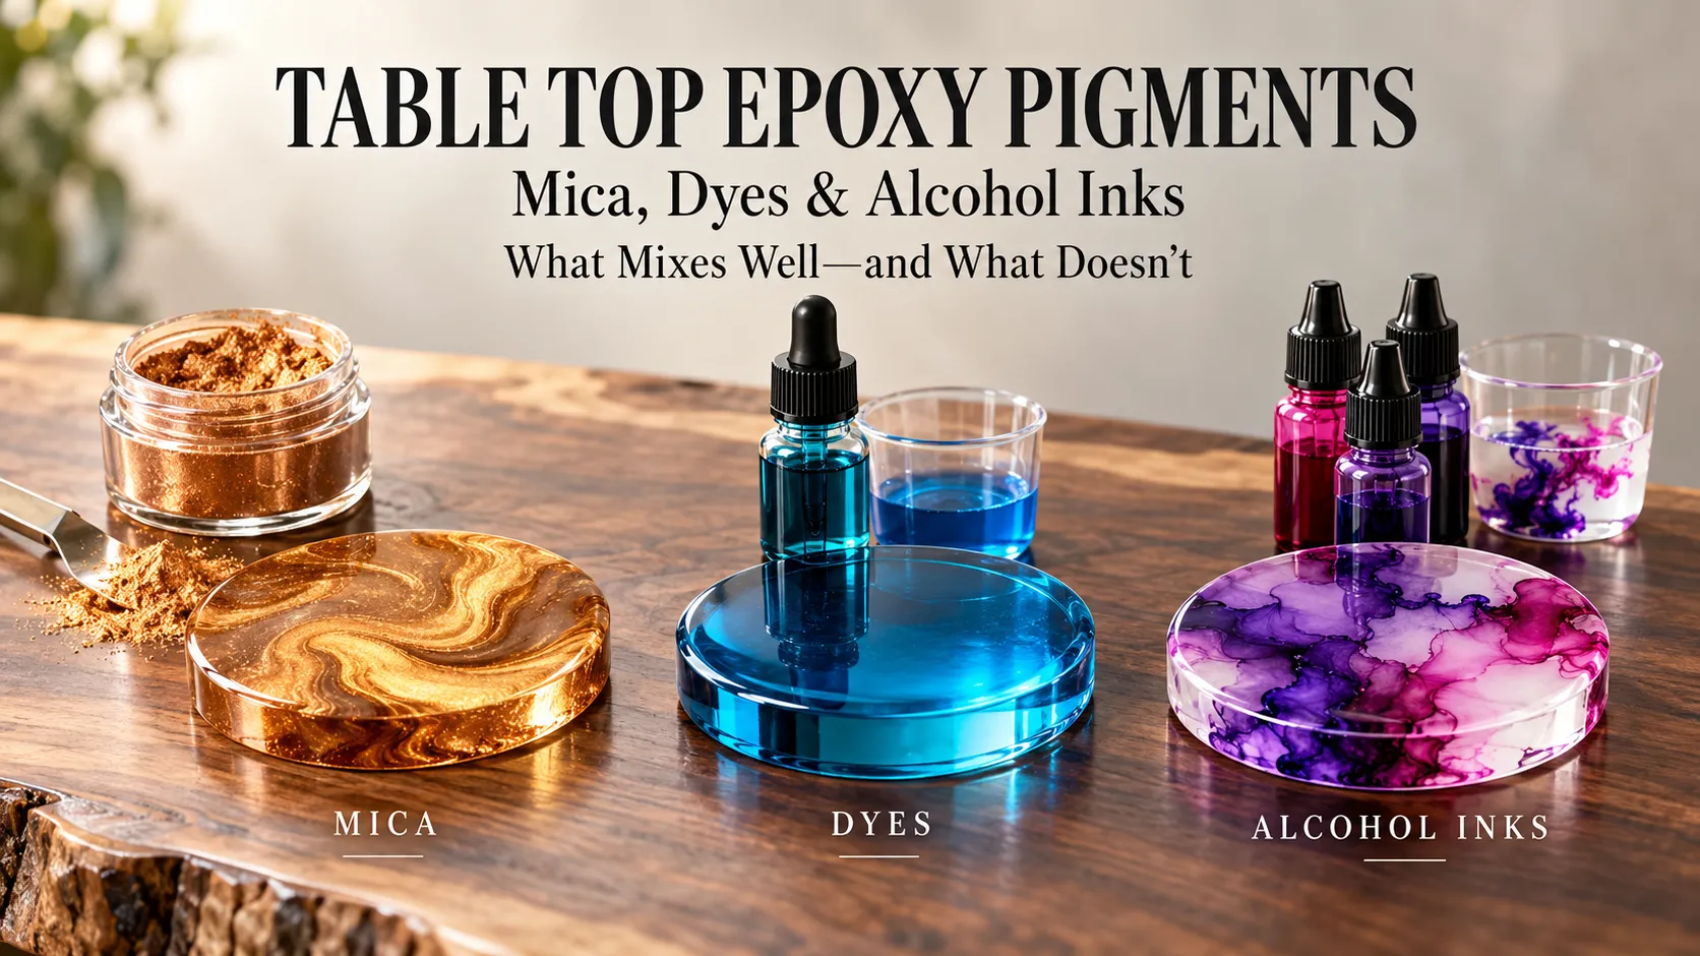
Table Top Epoxy Pigments: Mica, Dyes and Alcohol Inks — What Mixes Well and What Doesn’t

Most color failures in epoxy get blamed on the resin. They shouldn’t be. When a table top comes back cloudy, tacky in patches or two shades off the sample, the culprit is usually the colorant — the wrong type, too much of it, or one that never belonged in epoxy in the first place.

If you buy or sell table top epoxy in volume, this matters twice. Your customers will color the resin themselves, and every failed pour lands as a complaint on your desk. A good epoxy resin manufacturer can tell you which colorants have been tested with a given formula. A bad one shrugs.

This guide covers the table top epoxy pigments that work, the ones that don’t, and the loading limits that keep a pour curing hard and clear. Treat the numbers as starting points — the TDS for your specific resin always wins.

Table Top Epoxy Pigments

Why colorant choice changes more than color

Epoxy is a two-part chemical reaction. Anything you stir in either joins that reaction or interferes with it. Pigment particles raise viscosity and hold onto air. Solvents in some inks evaporate during cure and leave haze behind. Water — even a few drops — reacts with the hardener and turns the surface cloudy or sticky.

So colorants split into two groups: those made for epoxy, and those that merely look good in a cup of wet resin. Only the first group survives a full cure and years of daily use. Any epoxy resin manufacturer worth working with will have sorted its approved list into exactly those two piles.

Five colorants compared

Loading rates below are by weight of mixed resin unless noted. They hold for most table top epoxy; deep pour epoxy and UV resin follow different limits, covered further down.

ColorantBest forTypical loadingWatch out for
Epoxy pigment pasteSolid, opaque colors — black, white, solid blues and greens1–5%Heavy loading thickens the mix and can slow cure. Opaque color hides depth, so it is wrong for river tables.
Mica powderPearl, metallic and shimmer effects1–5% (up to about 8% for dense metallics)Settles in thin, low-viscosity mixes. Clumps if dumped in dry. Holds micro-bubbles.
Transparent epoxy dyeTranslucent “water” effects in river tables0.5–2%Looks darker in thick pours. Cheaper dyes fade in sunlight.
Alcohol inkCells, marbling and accent veinsA few drops per 8 oz (about 240 ml); stay under 2%Solvent causes haze or soft spots when overused. Most inks have poor lightfastness.
Acrylic paintNot recommended as a base colorUnder 3% if used at allWater content clouds the cure and weakens the bond.

Pigment paste: the safe default

If you want one colorant that works almost every time, use a pigment paste made for epoxy. The pigment is already dispersed in a resin carrier, so it blends without clumps and brings no water or solvent into the mix. Of all table top epoxy pigments, it is the one with the fewest ways to go wrong.

Start at 2% and adjust. Past 5%, the mix gets noticeably thicker, bubbles stay trapped longer and cure can slow. Opaque white is the heaviest offender — titanium dioxide is dense and needs more mixing time than most people expect.

One production habit worth copying: add the colorant to the resin side first, mix until the color is uniform, then add the hardener. Coloring after the two parts are combined eats into your working time and tends to leave streaks.

Mica powder: effect, not coverage

Mica gives table top epoxy its pearl and metallic look, but it doesn’t cover the way a paste does. Light passes through a mica-tinted pour, so the color you see depends on thickness, lighting and whatever sits underneath.

Pre-wet it. Stir the powder into a small amount of resin until it forms a smooth paste, then fold that into the batch. Dumped in dry, mica forms clumps that no amount of stirring will break. Stir slowly, too — fast mixing whips in micro-bubbles, and mica particles cling to them. And pour promptly. In thin coats, heavier metallic mica drifts toward the bottom within minutes. That is a feature if you want a shimmering base layer and a defect if you don’t.

For a river table, mica in the water channel works at 1–2%. Above that, the channel goes from translucent to cloudy.

Alcohol inks: use sparingly

Alcohol inks create the cells and feathered edges you see in ocean-style pours. They work because the alcohol carrier spreads fast and pushes resin aside. That same carrier is the problem.

Alcohol is a solvent. A few drops per 8 oz (about 240 ml) do no harm. Past roughly 2% by volume, you risk haze, soft spots and a longer cure. Most alcohol inks also fade — direct sun can wash bright pinks and reds noticeably within months. For tables near windows or outdoor counters, switch to mica or an epoxy-rated dye.

Use alcohol ink as an accent in a thin top layer. Never as the base color of the pour.

Colorants that don’t belong in epoxy

Some products keep turning up in DIY tutorials and shouldn’t. Food coloring, watercolor and other water-based products bring water into the mix — the hardener reacts with it, and the surface clouds or stays tacky. Oil-based paints and crayon shavings can interfere with cure. Cheap craft glitter sometimes bleeds dye into the resin. None of these were built to sit inside a two-part reaction.

How colorants behave in different systems

Table top epoxy. Coats run about 1/8 to 1/4 inch (3–6 mm), so color reads strongly even at low loading. There is rarely a reason to push a paste past 3%.

Deep pour epoxy. Pours go up to about 2 inches (5 cm) per layer, and transparent dyes deepen with thickness. A shade that looks right in a 1/8-inch test cup can look nearly black at full depth. Test at the real pour depth, not in a shallow cup.

UV resin. Opaque pigments block UV light, so the layer under the surface never cures. Stick with transparent dyes at 0.5% or less and cure in thin layers.

A five-step test before any production run

  1. Mix a 100 g (about 3.5 oz) test batch at your planned loading.
  2. Pour it at the real thickness — a cup filled to the depth of the final pour, not a thin smear.
  3. Wait out the full cure — typically 72 hours for table top epoxy, or whatever the TDS specifies. Don’t judge at 24 hours.
  4. Check the sample: press a fingernail into an edge, then look for tack, haze and specks.
  5. Leave one sample in direct sunlight for a week and see whether the color shifts.

What to ask your epoxy resin manufacturer

If you source table top epoxy for resale or private label, ask three questions before approving a formula. Which colorant types has it been tested with? What loading limit do they recommend before cure suffers? And can they supply a compatibility sheet you can pass on to customers?

At Jinhua Resin, we are an epoxy resin manufacturer supplying table top epoxy, deep pour epoxy and UV resin under OEM and private label programs. If colorant compatibility matters for your product line, tell us which pigments your customers use and we’ll talk through what to test.

FAQ

How much pigment can I add to table top epoxy?

Most epoxy pigment pastes work between 1% and 5% by weight. Beyond about 6%, the risk of a soft or slow cure rises. Check the TDS for your resin.

Can I mix mica and alcohol ink in the same pour?

Yes, but in separate layers — mica in the base, alcohol ink as a thin accent on top. Mixed together in one cup, the solvent tends to clump the mica.

Why did my colored epoxy turn cloudy?

The usual causes are water contamination, too much solvent-based ink, or too much pigment. A damp mixing cup is enough to do it.

Does color change cure time?

Heavy loading slows cure by diluting the reaction. Stay within the recommended range and the effect is small.

Epoxy Resin Outdoors (2)

Can You Use Epoxy Resin Outdoors? UV, Rain and Weather Resistance Explained

Epoxy turns up everywhere: river tables, countertops, wood coatings, concrete floors, industrial surfaces. It sticks hard, cures hard, shrugs off most chemicals and looks great doing it. Then someone asks the obvious question. Will it survive a summer on the patio?

Short answer: yes, but not every epoxy is built for it. Using epoxy resin outdoors works when the formulation, the surface prep and the top protection all match the exposure. Rain is rarely what ruins a job. Sunlight is.

A fully cured epoxy handles water well. A standard grade, though, will yellow, dull and chalk if it sits under continuous UV. So “waterproof” is only one item on the checklist. You also need to ask about UV, temperature swings, freeze-thaw, substrate movement, and how many years the surface has to last. This guide takes them one at a time, written from the formulation side by an epoxy resin manufacturer.

Epoxy Resin Outdoors (2)

Where Epoxy Works Outside

Epoxy holds up in plenty of exterior jobs: wooden tables and patio furniture, decorative wood, concrete surfaces, signs, marine parts, composites and exterior repairs. But a craft-grade clear epoxy made for indoor tabletops and an industrial coating engineered for weather are two very different products, even when both are sold as “epoxy.”

The good results all follow the same pattern: the right resin, a properly prepared surface, correct application, and UV protection on top.

Is Epoxy Resin UV Resistant?

Standard epoxy is not UV stable. Sunlight slowly attacks the cured polymer, and the damage shows up as yellowing, a cloudier look, lower gloss, a chalky surface, color drift and, eventually, surface breakdown.

None of this happens overnight. How fast it goes depends on the formulation, whether UV stabilizers are included, sunlight intensity, daily hours of exposure, local climate, color and whether there is a topcoat. Clear epoxy shows the change first, because even a faint yellow tint is obvious against a clean finish. Pigmented epoxy hides the shift. It does not stop it.

Why Epoxy Turns Yellow in the Sun

The mechanism is photo-oxidation. Ultraviolet energy breaks down the aromatic structures found in most standard epoxy chemistry, and the fragments absorb light differently, which reads as yellow or amber. Heat, oxygen, hardener chemistry and film thickness all speed it up.

Many modern formulations carry UV absorbers or hindered amine light stabilizers to slow the process. Read that carefully, though: UV resistant is not UV proof. A stabilized epoxy stays clear longer than a basic one. Under continuous direct sun, it will still change. If color stability matters to the project, plan on a UV-stable topcoat from the start.

Is Cured Epoxy Waterproof?

Once cured, epoxy has excellent water resistance. It forms a continuous film that keeps moisture out of porous materials like wood and concrete.

But the coating is only as good as its weakest point, and water always finds it. Cracks, pinholes, bare edges, joints, screw holes, damaged patches and badly prepared substrates are all entry routes. Coat only the top of a wooden table and rain will still get in through the underside, the edges and the joints. The wood swells, and the coating starts to lift.

Can Rain Damage Epoxy?

Fully cured epoxy: no, not from ordinary rain. Uncured epoxy: yes. Rain or heavy dew during cure can cause cloudiness, surface haze, blushing and uneven gloss.

Before any exterior application, check the air and substrate temperature, relative humidity, dew point, the rain forecast and the cure time the product needs. A common field rule is to keep the substrate at least 3°C (5°F) above the dew point. Do not judge readiness by touch, either. Touch-dry and fully cured are not the same thing. Most ambient-cure epoxies need around seven days at 25°C (77°F) to reach full cure, so follow the technical data sheet before exposing the surface to rain or standing water.

What Temperature Swings Do to Outdoor Epoxy

A patio table can be cool at dawn, scorching by mid-afternoon and cool again at sunset. That daily cycle makes both the epoxy and the material underneath expand and contract, usually at different rates. Wood adds another variable because it also moves with moisture.

Repeated cycling can lead to cracking, delamination, lost adhesion and edge lift. The risk applies to wood, metal, concrete and composites alike, which is why the coating system has to be chosen for the substrate and the climate together.

Hot Sun: UV Plus Heat

Sunlight hits epoxy twice, once with UV and once with heat. A dark surface in direct sun can run far above the air temperature. On a 35°C (95°F) day it can pass 65°C (150°F).

That matters because many ambient-cure epoxies have a glass transition temperature (Tg) somewhere in the 45–65°C range, so check the datasheet for the exact figure. As the surface approaches Tg, the epoxy softens. It dents more easily, can deform and loses hardness. Design for the expected surface temperature, not the number on the weather app, and check the recommended service temperature before committing.

Can Epoxy Survive Freezing Weather?

Cured epoxy generally tolerates cold well. The harder test is freeze-thaw. Water that has worked into cracks, pores or joints expands when it freezes, and repeated cycles stress both the coating and the substrate. Exterior concrete is especially exposed.

Application temperature is a separate problem. Mixing and pouring at very low temperatures gives thicker material, poor leveling, weak wetting and slow or incomplete cure, even when the cured product could have handled the cold just fine. Keep the two specs apart: application temperature (most epoxies work best at roughly 18–30°C, or 65–85°F) and service temperature after cure.

Epoxy on Outdoor Wood

Wood is one of the better outdoor uses. Epoxy seals the pores and cuts moisture uptake on tables, benches, signs, marine timber and furniture. The wood needs to be dry, clean, sanded, free of oil and structurally sound before anything goes on.

Spend the extra time on edges, joints, cracks and end grain, because that is where wood drinks water. For long-term sun exposure, add a compatible UV-resistant exterior finish over the epoxy. The epoxy does the sealing and bonding; the finish takes the sunlight.

Epoxy on Outdoor Concrete

Epoxy can work on some exterior concrete, but four things need attention first.

Moisture vapor. Water travels up through a slab. Even if the epoxy sheds rain from above, vapor pressure from below can cause blisters and delamination, and a vapor barrier may be needed. UV. Standard epoxy yellows and chalks under sun. Thermal movement. Exterior slabs heat, cool and crack. Slip. Smooth epoxy turns slick when wet, so walking surfaces need anti-slip aggregate or texture.

Because of all that, exterior floor systems often use epoxy as the primer or build coat and put a more UV-stable material on top.

Epoxy vs Polyurethane vs Polyaspartic for Exterior Use

These materials are usually partners, not substitutes. Epoxy brings adhesion, hardness and build thickness. Polyurethane and polyaspartic coatings bring better UV stability and color retention. The common exterior system is an epoxy base coat with a UV-stable topcoat.

PropertyEpoxyPolyurethanePolyaspartic
UV stabilityLow to moderate (standard grades)GoodGood to very good
Bond to prepared concreteExcellentModerate; usually a topcoatGood
HardnessHighModerateHigh
FlexibilityLowHigherModerate
Cure speedSlow to moderateModerateFast
Typical exterior rolePrimer or build coatUV topcoatUV topcoat, quick return to service

Treat the table as a general guide. Performance varies by formulation, and the word “polyaspartic” on a label does not guarantee weather resistance. Ask for technical data on the actual system, and confirm layer compatibility and recoat windows before you order.

How to Make Outdoor Epoxy Last Longer

Pick the right resin. Choose a product made for your substrate and exposure. Ask for data on UV resistance, water resistance, service temperature, adhesion, chemical resistance and recommended topcoats.

Prepare the surface. The substrate should be clean, dry, free of oil and dust, and sanded or mechanically profiled. Poor prep will sink a high-quality epoxy.

Seal every weak spot. On wood and other porous materials, that means edges, corners, joints, holes, cracks and undersides. Water goes for the weakest point.

Hit the film thickness. A coat that is too thin or uneven protects less than you think. Follow the coverage rate on the datasheet.

Let it fully cure. No rain, standing water, heavy use or big temperature swings until the recommended cure stage.

Add UV protection. For direct sun, use a compatible polyurethane or polyaspartic topcoat. Any epoxy resin manufacturer worth working with will tell you which topcoats suit its system.

Inspect regularly. Look for cracks, scratches, chalking, gloss loss, delamination and edge damage. Small repairs made early keep moisture away from the substrate.

How Long Does Epoxy Last Outdoors?

There is no universal number. A covered table and an uncovered surface baking in daily sun age at completely different rates. An exterior industrial floor with vehicles and chemicals needs a different system from a decorative garden bench. Service life comes down to formulation, UV exposure, climate, moisture, temperature cycling, substrate movement, prep quality, film thickness, wear, maintenance and topcoat.

So skip “how many years will it last?” and ask a better question: what will this surface actually be exposed to, and what system matches that?

Frequently Asked Questions

Can epoxy resin stay outside?

Yes, suitable systems can. Standard epoxy may yellow or lose gloss under prolonged UV, so extra UV protection is often needed.

Is epoxy resin waterproof in the rain?

Fully cured epoxy resists water well. Cracks, pinholes, joints and unsealed edges can still let water reach the substrate.

Does epoxy resin yellow in sunlight?

Many standard clear epoxies do, gradually. UV stabilizers slow it, and a compatible UV-resistant topcoat slows it further.

Can epoxy be used on outdoor wood furniture?

Yes. It seals the wood and reduces moisture uptake, but furniture in direct sun is better with a UV-resistant finish on top.

Can epoxy be used on an outdoor patio?

It depends on the concrete condition, moisture level, sun exposure, temperature range and slip requirements. A multilayer system with a UV-stable topcoat usually beats exposed standard epoxy.

Is epoxy UV proof?

No standard epoxy should be treated as UV proof. Some formulations resist UV better, but prolonged sunlight still affects most systems.

Can epoxy survive winter?

Cured epoxy can perform in cold climates if the whole system is designed for it. Freeze-thaw cycling, substrate moisture and movement are the things to plan around.

Final Thoughts: Can You Use Epoxy Resin Outdoors?

Yes, but rain is the smallest part of the answer. A well-chosen, fully cured epoxy gives you strong adhesion, water resistance, surface sealing, hardness and chemical resistance. What outdoor exposure adds is UV, yellowing, high surface temperatures, temperature cycling, freeze-thaw and substrate movement.

For covered furniture, protected wood, certain concrete jobs, composites and repairs, epoxy is a solid choice. For surfaces in strong direct sun, add UV protection. In many professional systems, epoxy is the bonding and build layer, and a UV-resistant polyurethane or polyaspartic topcoat handles the weather.

Jinhua Resin is an epoxy resin manufacturer supplying systems for tabletop coatings, deep casting, DIY projects, wood applications, composites, flooring and industrial use, with OEM and private-label formulation available. Check UV exposure, water resistance, service temperature, substrate, film thickness and long-term weather before you pick a formulation, and outdoor results get a lot more predictable.

Epoxy Resin Heat Resistance

Epoxy Resin Heat Resistance: What Temperature Can It Actually Take?

Countertops, river tables, coatings, adhesives, electrical encapsulation, composites — epoxy shows up everywhere because it’s strong, versatile, and takes an incredible amount of abuse. But heat is where things get complicated. The moment epoxy sits near hot pans, machinery, direct sunlight, or high processing temperatures, one question comes up constantly: how heat resistant is epoxy resin, really?

There’s no clean answer. Resin chemistry, hardener choice, cure schedule, formulation, and end use all shape how a given epoxy handles heat. A basic clear craft resin might start softening well before a purpose-built high-temperature system even notices the heat. Marketing copy that just says “heat resistant” glosses over all of that — and it’s exactly the kind of vague claim that gets buyers into trouble.

This guide breaks down what epoxy resin heat resistance actually means, what happens when cured epoxy gets pushed past its limits, and how to pick the right resin for countertops, casting, industrial parts, and everything in between.

Epoxy Resin Heat Resistance

Yes, But It Depends

Fully cured epoxy resin does offer real heat resistance — that part’s true. What varies is how much.

General-purpose resins made for crafts, furniture, and coatings are built around moderate service temperatures. They’re not designed to shrug off industrial heat loads. Specialty high-temperature epoxy systems exist precisely because standard formulations can’t keep up in more demanding environments.

Before comparing products, it helps to know these aren’t interchangeable terms:

  • Service temperature
  • Short-term heat exposure tolerance
  • Continuous operating temperature
  • Glass transition temperature (Tg)
  • Heat deflection temperature (HDT)
  • Thermal degradation point

An epoxy that survives a quick brush with a hot object might fail completely under sustained exposure to that same temperature. So instead of asking “what temperature can epoxy handle,” the more useful question is: what temperature can this epoxy handle, for how long, in this application?

So What’s the Actual Temperature Limit?

There isn’t one universal number, but general-purpose cured systems typically land somewhere in the 50–80°C (122–176°F) range for continuous service. Formulated high-temperature epoxies can push past 100°C (212°F), and specialized industrial systems go considerably higher still.

Treat those figures as ballpark, not gospel. Real-world performance depends on resin chemistry, the hardener, the mix ratio, cure temperature, whether the part gets post-cured, any fillers involved, how long the heat exposure lasts, and whether the piece is under mechanical load at the same time. When heat resistance actually matters for a project, pull the Technical Data Sheet. Don’t guess from the label.

Glass Transition Temperature (Tg) — Why It Matters More Than “Heat Resistant”

Tg gets thrown around a lot, and it’s worth actually understanding.

It’s not a melting point. Epoxy is a thermoset — once it cures, it forms a crosslinked network that doesn’t revert to liquid resin no matter how hot it gets. Tg instead marks the range where cured epoxy shifts from a hard, glassy state into something softer and more rubber-like.

Near or past Tg, expect the material to lose stiffness, flex more, carry less load, and become more prone to deformation. A part can look completely fine at an elevated temperature while its actual mechanical strength has already dropped significantly. That’s why “heat resistant to 100°C” tells you far less than the Tg number does — especially for anything structural.

Heat Deflection Temperature (HDT)

HDT is a different measurement: how a material behaves under a specified load as temperature climbs. It matters most for parts that need to hold their shape while carrying weight or stress.

Tg and HDT are related but not the same test, and not interchangeable. When comparing two epoxy products’ spec sheets, confirm you’re looking at the same type of measurement rather than assuming every number on the page means the same thing.

What Actually Happens When Epoxy Gets Too Hot

Push cured epoxy past its intended range and a few things tend to happen, sometimes in sequence.

It softens. As temperature nears or crosses Tg, the surface gets noticeably less rigid — a tabletop, for instance, becomes easier to dent with a hot pot.

It deforms under load. If the piece is bearing weight while hot, it can gradually change shape. This is a real concern for structural components and composites specifically.

It loses mechanical performance. Stiffness, strength, adhesion, and dimensional stability all drop at elevated temperatures — sometimes without any visible sign that something’s wrong.

It discolors. Clear or light-colored epoxy can yellow or darken under excess heat.

It cracks or delaminates. Repeated heating and cooling makes materials expand and contract. If the resin and substrate don’t expand at the same rate, thermal cycling can eventually crack the surface or pull it loose from the substrate.

It degrades. At high enough temperatures, epoxy undergoes actual chemical breakdown — not the temporary softening near Tg, but permanent damage. Once that happens, the material doesn’t recover its original properties on cooling.

Does Epoxy Melt?

Not in the way people usually mean. Thermoplastics soften, melt, and can be reshaped and reheated indefinitely. Epoxy can’t do that once it’s cured — the crosslinked network that forms during curing is permanent.

Push it hard enough with heat and it’ll soften, deform, lose strength, discolor, or eventually char and break down chemically. But it won’t liquefy back into resin. “Melting” just isn’t the right word for what’s happening.

Table Top Epoxy and Heat: What’s Realistic

This is where heat resistance gets personal for most buyers, because table top epoxy surfaces deal with coffee cups, plates, cooking containers, and warm serving dishes on a near-daily basis.

A properly cured tabletop surface handles normal household temperature swings and moderate warmth without issue. What it can’t handle is a pan straight off the stove or out of the oven — that’s often far hotter than any standard decorative epoxy’s service range, and setting it down directly risks soft spots, imprinting, discoloration, or permanent gloss damage. A trivet or heat pad solves the problem entirely and costs nothing to use.

Deep Pour Epoxy: Different Problem, Different Solution

Deep pour epoxy gets formulated to deal with a completely different heat challenge: the exothermic reaction that happens during curing, not after.

Pour too much resin at once and heat builds up inside the casting faster than it can escape. That leads to rapid uncontrolled curing, bubbling, yellowing, cracking, internal stress, and in bad cases, smoke. Deep pour systems slow the reaction down specifically so heat has time to dissipate during a thick pour.

Here’s the catch people miss: managing exotherm during cure and having high heat resistance after cure are two completely separate properties. A deep pour resin engineered for a thick river-table casting might have roughly the same post-cure service temperature as any other decorative epoxy. Always check the cured resin’s thermal specs on their own — don’t assume a low-exotherm formulation implies high heat tolerance.

Industrial Applications Raise the Stakes

Motors, electrical components, machinery, composite parts, encapsulation, industrial adhesives — these environments push epoxy far beyond anything a countertop sees. Here, thermal performance has to work alongside mechanical and chemical demands simultaneously.

A high-temperature epoxy in an industrial setting needs to hold onto adhesion, dimensional stability, electrical insulation, mechanical strength, and chemical resistance through repeated heating and cooling cycles — not just survive one heat spike. Picking whichever product advertises the highest number isn’t a strategy. The full operating environment needs evaluation, not a single spec.

Post-Curing: Does It Actually Improve Heat Resistance?

Sometimes. Post-curing means running cured or partially cured epoxy through a controlled elevated-temperature schedule afterward. Done right, on a formulation designed for it, this can push the polymer network toward a higher degree of cure and raise Tg or other thermal properties.

But this only works when the product is built for it. Heating a standard epoxy on your own doesn’t turn it into a high-temperature resin — it might do nothing, or it might cause problems. If post-curing is viable, the manufacturer needs to specify the temperature, duration, ramp rate, and cooling procedure. For production runs, following that schedule exactly is what makes performance consistent from batch to batch.

Does Thickness Change Heat Resistance?

Two different answers depending on when you’re asking.

During curing, yes — a thick pour holds onto exothermic heat far more than a thin coating does. A resin built for a 3mm coat shouldn’t get poured at 50mm; the heat buildup alone can cause real problems.

After curing, it’s murkier. A thicker cured section doesn’t automatically have a higher Tg or service temperature — that’s set by the chemistry and cure state, not the dimensions. That said, thick and thin sections do heat and cool at different rates in the real world, which can still affect how they actually perform in use.

What Actually Determines Heat Resistance

A handful of variables do most of the work.

Resin and hardener chemistry sets the crosslinked structure, which is the main reason thermal performance varies so much between products. Getting the mix ratio right matters too — too much or too little hardener doesn’t speed up cure or improve heat resistance, it just prevents the resin from curing fully. A partially cured epoxy will underperform a fully cured one on heat resistance every time, and post-curing (when the formulation supports it) can push Tg higher still. Fillers can shift thermal behavior and heat transfer characteristics depending on what’s used. And exposure time changes everything — a resin that survives a brief touch at a given temperature might fail completely if held there for hours or days. Add mechanical load on top of heat, and the margin for error shrinks further.

Epoxy vs. Polyurethane on Heat

Neither wins outright — both chemistries can be engineered across a range of temperatures.

Epoxy tends to bring strong adhesion, hardness, dimensional stability, chemical resistance, and solid composite performance to the table. Polyurethane often counters with more flexibility, better abrasion and impact resistance, and, in the right formulations, good UV stability. When temperature matters for a specific project, compare actual technical data between the two products rather than assuming one chemistry automatically beats the other on heat.

Choosing a Heat-Resistant Epoxy: A Practical Checklist

Before buying, work through these:

  1. What’s the normal operating temperature the finished piece will see most of the time?
  2. What’s the realistic maximum — occasional spikes, hot objects, nearby machinery?
  3. How long does that exposure actually last? Ten seconds at 100°C and continuous operation at 100°C are entirely different problems.
  4. Will the part be under mechanical load while it’s hot?
  5. Check the Tg and HDT numbers — they tell you far more than a vague “heat resistant” claim ever will.
  6. Confirm the cure schedule. Some systems only hit their rated thermal performance after a full cure or post-cure.
  7. Think about the substrate. Resin and substrate rarely expand at the same rate as temperature shifts.
  8. Ask for the TDS before any bulk or commercial purchase. This one step avoids most heat-related failures downstream.

FAQ

What temperature can epoxy resin withstand? It depends entirely on the formulation. General-purpose systems handle moderate service temperatures; specialized high-temperature epoxies go considerably higher. The TDS is the only reliable source for a specific product’s limits.

Is epoxy resin safe for hot coffee mugs? Generally yes for normal household warmth, but prolonged contact with very hot items can still leave marks on some formulations. A coaster removes the risk entirely.

Can you put a hot pan on an epoxy countertop? Better not to. Cookware straight from a stove or oven usually runs hotter than a standard decorative epoxy’s service range.

Does epoxy melt in heat? No — it’s a thermoset, not a thermoplastic. Excessive heat causes softening, deformation, discoloration, or chemical degradation, not melting.

Does epoxy get soft when heated? Yes, particularly as it approaches or crosses its glass transition temperature.

Can epoxy withstand boiling water? Some formulations tolerate brief exposure near boiling; others soften or lose performance. It depends on the specific resin, its cure state, and how long the exposure lasts.

Is deep pour epoxy more heat resistant than other types? Not automatically. Deep pour formulations manage exothermic heat during a thick cure — that’s a separate property from post-cure service temperature.

The Bottom Line

There’s no single number that defines epoxy resin heat resistance across every product. Standard systems handle moderate heat just fine; purpose-built formulations exist for the situations that need more.

What actually determines performance: resin and hardener chemistry, Tg, HDT, full cure, post-cure schedule where applicable, exposure duration, mechanical load, and the substrate underneath. For countertops, river tables, crafts, and general coatings, standard epoxy usually covers what’s needed within its intended range. For machinery, electronics, high-temperature composites, or industrial parts, that’s a job for an engineered high-temperature system.

Don’t buy on a single advertised number. Pull the TDS, and figure out whether that number describes continuous service, a brief spike, Tg, HDT, or something else entirely — they’re not the same claim wearing different labels.

Jinhua Resin supplies epoxy systems for tabletop coatings, deep pour epoxy, DIY projects, wood applications, composites, and industrial use, with OEM and private-label options available across markets. Matching the right formulation to working time, viscosity, pour thickness, cure schedule, hardness, and thermal requirements is what makes performance reliable once a project moves from spec sheet to real-world use.