Epoxy Resin Hardener

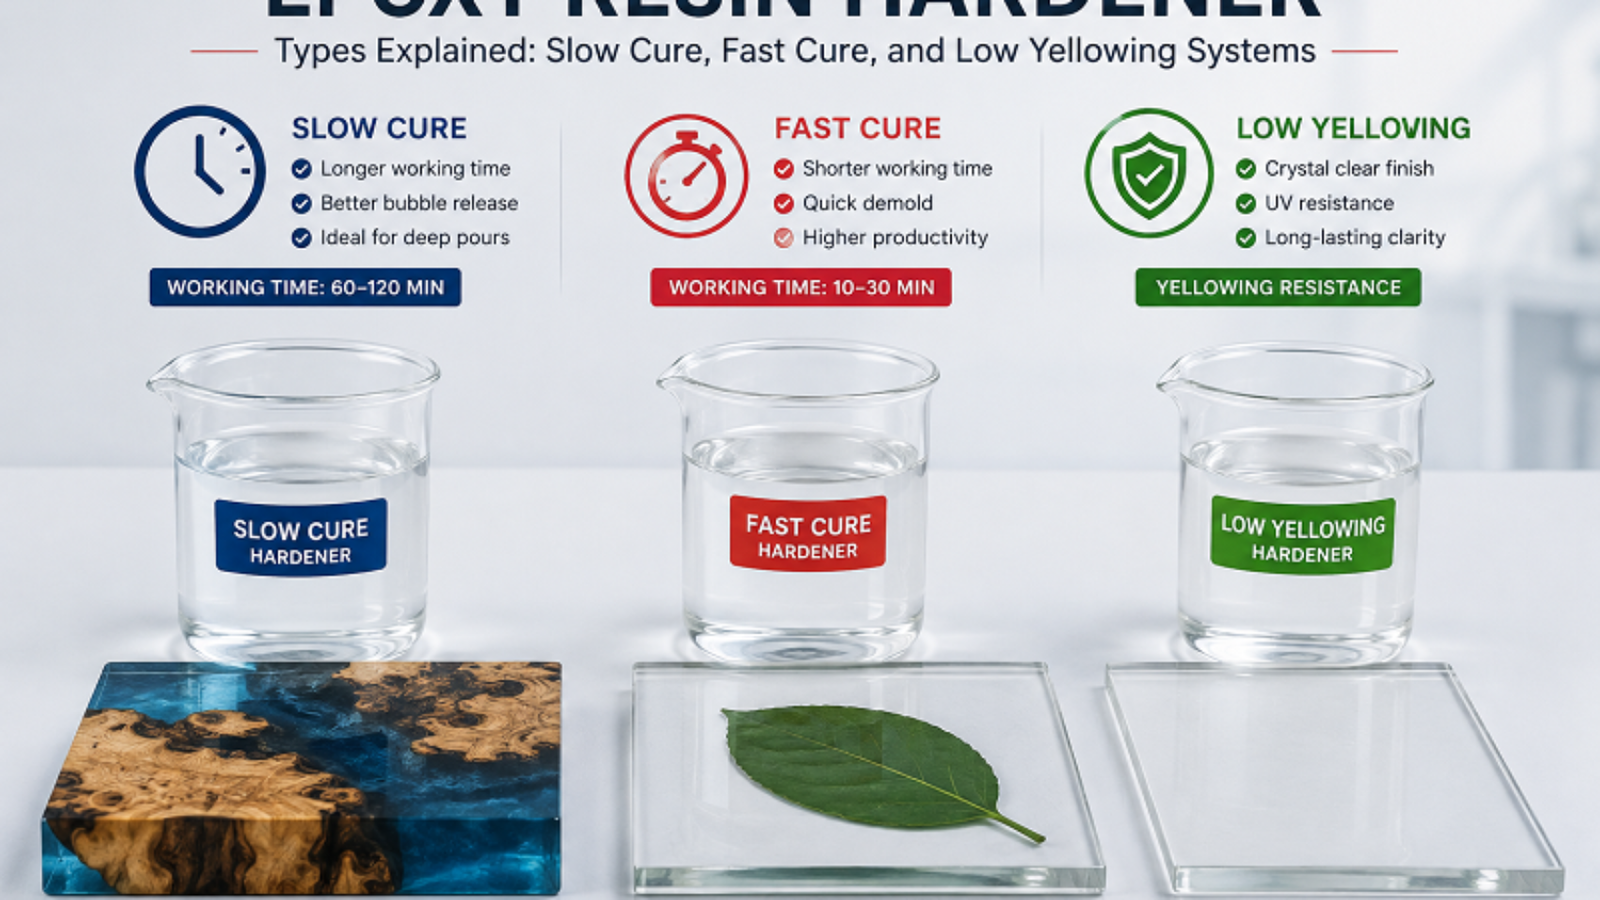
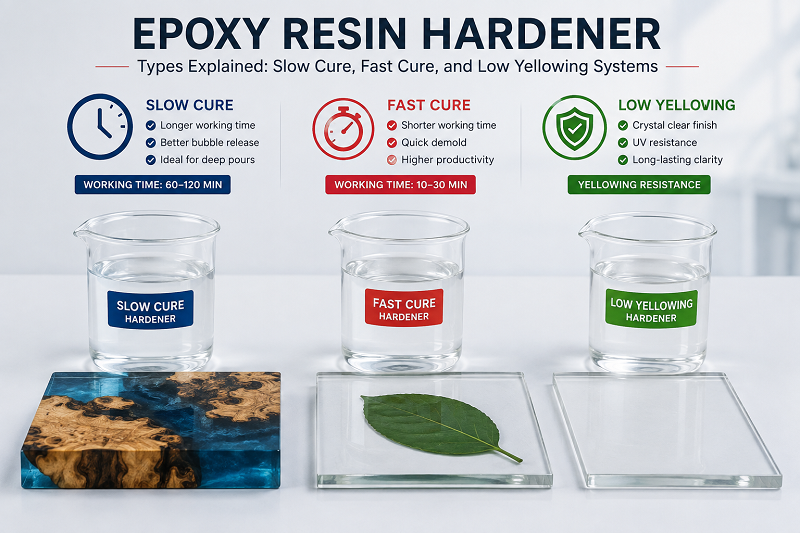
Epoxy Resin Hardener Types Explained: Slow Cure, Fast Cure, and Low Yellowing Systems

Most conversations about epoxy resin focus on the resin itself. What actually decides whether a project succeeds is the hardener.

Many buyers evaluating an epoxy resin manufacturer spend most of their effort comparing resin viscosity, mix ratios, and pricing, then treat the hardener as an afterthought — a costly assumption. The hardener governs cure speed, heat output, clarity, and long-term color stability. Get the resin right and the hardener wrong, and the same problems keep showing up: cracked deep pours, cloudy tabletops, coatings that yellow before their first year is out. This article walks through the three hardener categories that matter most to B2B buyers — slow cure, fast cure, and low yellowing — and where each one actually belongs.
Epoxy Resin Hardener

Hardener Chemistry Decides the Outcome

Nearly all epoxy hardeners are amine-based — aliphatic amines, cycloaliphatic amines, or amine adducts. The amine reacts with the epoxide groups in the resin to build a cross-linked polymer network. The backbone structure of that amine determines three things: how fast the reaction proceeds, how much heat it releases at peak (exotherm), and how the cured polymer behaves under UV exposure over time.

This is exactly where hardener selection tends to go wrong, and where working with an experienced epoxy resin manufacturer actually earns its keep — because the wrong amine chemistry rarely shows up right away. A deep pour can look fine at 24 hours and still develop stress cracks by 72 hours, because the hardener released heat too fast, too early. A tabletop can look glass-clear on day one and turn amber within six months, because the hardener was never engineered for UV resistance. Buyers sourcing for resale or private label need tested performance data upfront — not a customer complaint after the fact.

Slow Cure Hardeners: Built for Mass and Depth

Slow cure hardeners extend working time and hold down peak exotherm, which is why they’re the standard choice for deep pour epoxy — river tables, thick castings, and any single-layer pour beyond roughly 1 inch (2.5 cm).

The logic is simple: slow cure hardeners rely on bulkier amine molecules or modified amine adducts that react more gradually with the epoxide. That keeps peak exotherm temperatures lower through a thick pour, which matters because runaway heat is the leading cause of cracking, yellowing, and bubbling in deep castings.

Typical figures for slow cure systems:

  • Pot time: 45–90 minutes at room temperature, varying with batch volume
  • Working time: Extended to 2–4 hours in some formulations, allowing large pours without premature gelling
  • Full cure: 3–7 days, sometimes longer past 2 inches of depth
  • Peak exotherm: Held low enough to avoid thermal cracking in single pours up to 2 inches

Buyers producing river tables, thick art castings, or large custom furniture should ask suppliers for the tested maximum pour depth per layer — this figure varies meaningfully between manufacturers and directly determines how many pour stages a project needs. A dependable epoxy resin manufacturer provides exotherm curves and maximum single-pour thickness data, not a generic “good for deep pour” claim.

Fast Cure Hardeners: Built for Turnaround

Fast cure hardeners sit at the other end of the spectrum. They use more reactive amine structures — typically lower-molecular-weight aliphatic amines — that speed up cross-linking. The trade-off is a shorter working window and higher exotherm per unit volume, which keeps fast cure systems limited to thin applications: coatings, small repairs, jewelry, and tabletop finishes under about 1/8 inch (3 mm).

Typical figures for fast cure systems:

  • Pot time: 5–20 minutes
  • Tack-free time: 2–4 hours
  • Full cure: 24–48 hours, well ahead of the multi-day cycle for slow cure systems
  • Thickness limit: Thin layers only — a thick pour run with fast cure hardener will overheat, cloud, or crack

Fast cure hardeners carry a direct commercial value wherever turnaround drives cost. Flooring contractors, repair shops, and small-batch coating operations all lean on fast cure for the same reason: faster demold and recoat times mean more jobs completed per week. For buyers evaluating OEM production schedules, cure speed is a real line item — a supplier that offers both fast and slow cure options can flex output around order volume instead of being locked into a single cure profile.

Low Yellowing Hardeners: Built for Clarity and Weather Resistance

This is the category that actually separates a solid epoxy resin manufacturer from one worth a long-term contract. Standard aromatic amine hardeners are inexpensive and cure predictably, but they yellow under UV exposure — sometimes within a matter of months. For tabletop epoxy, art resin, and anything sold on the strength of its clarity, that’s disqualifying.

Low yellowing hardeners get around this by using aliphatic or cycloaliphatic amines in place of aromatic ones. Aliphatic amine structures don’t contain the benzene ring that drives UV-triggered discoloration in aromatic systems, so the cured polymer holds its clarity considerably longer. Many formulations also add HALS (hindered amine light stabilizers) or UV absorbers into the hardener or resin package to push that resistance further out.

What buyers should specifically ask for:

  • Yellowing index data (ASTM D1925 or a comparable standard) tied to a defined number of UV exposure hours — an unverified “won’t yellow” claim isn’t worth much on its own
  • Aliphatic-to-aromatic amine ratio — a single spec that predicts long-term clarity far better than marketing language
  • UV stabilizer package — whether HALS or UV absorbers are included, and at what concentration

Table top epoxy and UV resin product lines depend almost entirely on this hardener category. A tabletop that yellows ruins the customer’s finished piece and the seller’s reputation at the same time — which is why buyers sourcing for resale should treat yellowing-resistance documentation as a mandatory part of supplier qualification, not an optional extra.

Comparing the Three Systems

PropertySlow CureFast CureLow Yellowing
Pot time45–90 min5–20 minVaries by base amine (often mid-range)
Full cure3–7 days24–48 hrs24 hrs–7 days
Best useDeep pour, river tablesCoatings, repairsTabletop, art resin, outdoor
ExothermLow, controlledHigher per volumeDepends on amine type
UV stabilityModerateModerateHigh

Worth noting: these three categories aren’t strictly separate in practice. Many production-grade hardeners are formulated to combine properties — a moderate-cure aliphatic amine hardener, for example, can deliver both workable pot time and strong yellowing resistance for tabletop use. This is exactly where OEM and private label buyers benefit from a direct formulation conversation instead of picking off a standard catalog.

Matching Hardener to Application

For buyers building out a product line, the decision usually comes down to three questions:

  1. How deep is the pour? Anything over an inch needs slow cure chemistry to manage exotherm. Thin coatings and repairs can run fast cure without cracking risk.
  2. Will the finished product see UV exposure? Indoor furniture that only catches occasional window light still benefits from low yellowing hardener. Outdoor coatings and countertops should treat it as a baseline requirement, not an upgrade.
  3. What’s the production turnaround target? Fast cure hardeners shorten the demold-to-ship window, which matters most for contract manufacturing under tight delivery deadlines.

An experienced epoxy resin manufacturer should be able to answer all three questions with test data rather than general reassurance, and should be able to adjust hardener ratios for climate — humidity and ambient temperature both shift working time and cure quality, sometimes significantly.

Working with a Manufacturer on Custom Hardener Formulations

Buyers running private label or OEM programs actually hold an advantage here: hardener systems can be tuned to the target market’s climate and application rather than sold as one formula for every customer. A supplier producing both deep pour epoxy and table top epoxy lines needs separate hardener formulations for each — slow cure with strong impact resistance for one, low yellowing with fast-enough turnaround for the other.

Jinhua Resin formulates hardener systems across all three categories in-house, which lets OEM and private label partners request adjusted pot times, exotherm profiles, or UV stability targets without switching suppliers between product lines. For buyers evaluating a long-term epoxy resin manufacturer relationship, that formulation flexibility — backed by real test data rather than marketing claims — is usually what settles the decision.

The Bottom Line

Slow cure, fast cure, and low yellowing hardeners aren’t interchangeable, and choosing by price alone tends to surface as a quality problem months down the line. Match the hardener to pour depth, UV exposure, and turnaround needs first — then evaluate suppliers on the data they’re willing to share, not the claims they’re willing to make.
Epoxy Resin Furniture

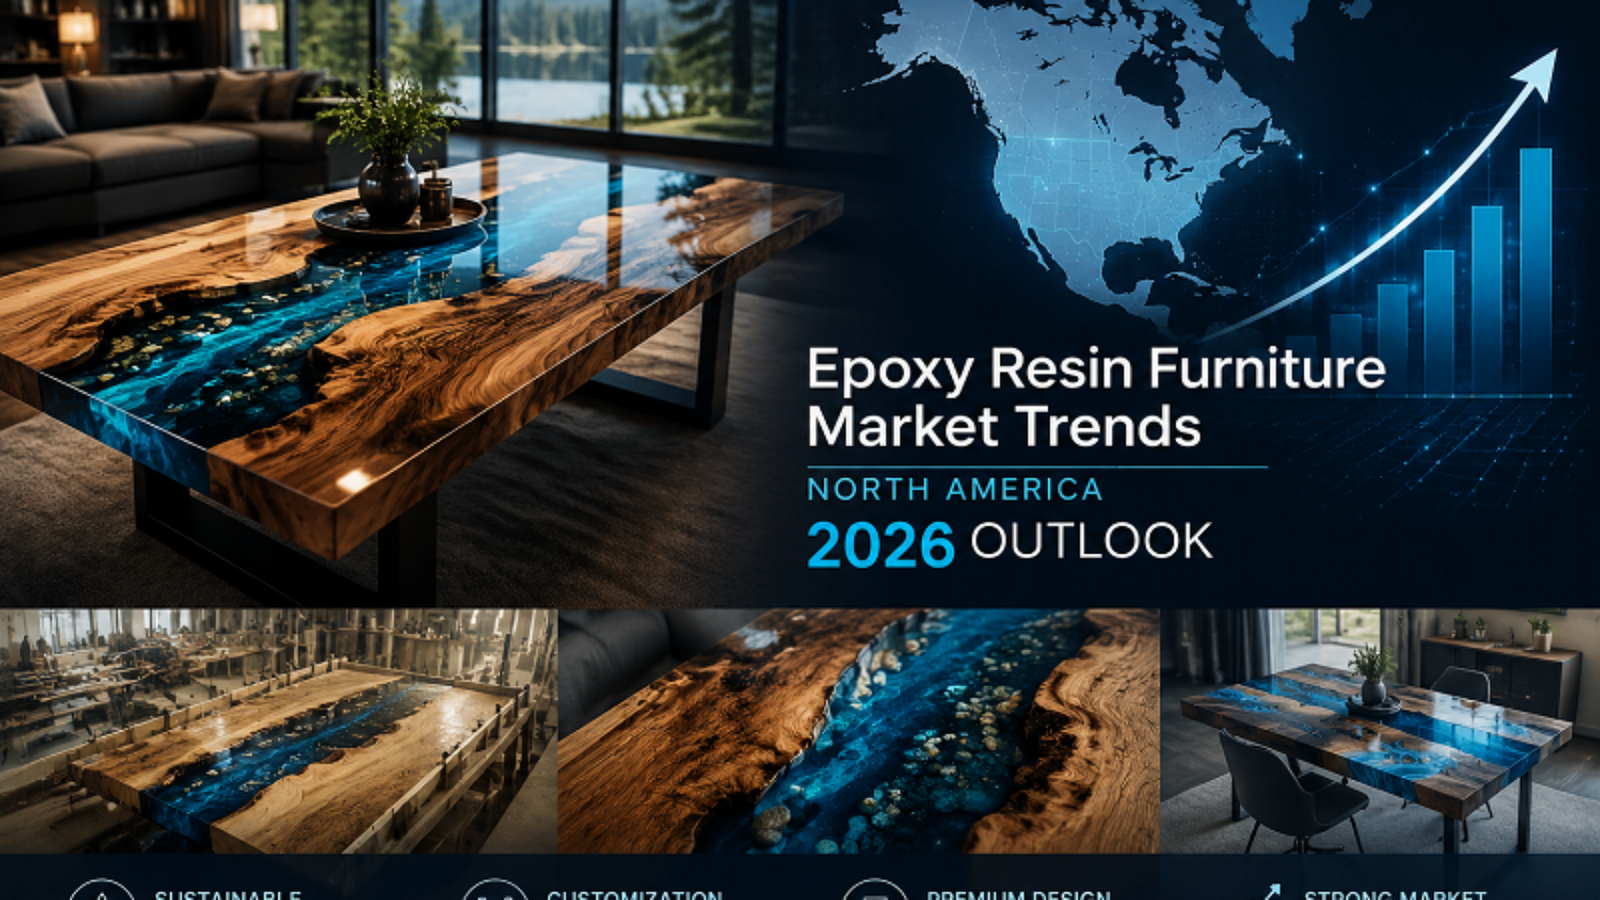
Epoxy Resin Furniture Market Trends in North America: 2026 Outlook

Resin furniture stopped being a niche maker product a few years ago. Walk into a mid-range furniture showroom in the US today, and there’s a decent chance a river table, a resin-and-wood coffee table, or an epoxy-topped counter is somewhere on the floor. For anyone sourcing from — or selling into — this category, it’s worth understanding where the North American market for Epoxy Resin Furniture is actually heading in 2026, not just where it’s been.

This isn’t a forecast pulled from a spreadsheet. It’s a practical read on the trends shaping demand, materials, and buyer expectations for Epoxy Resin Furniture across the US, Canada, and the wider North American market — useful whether you’re a distributor deciding what to stock, a furniture brand planning a new line, or a manufacturer trying to anticipate what buyers will be asking for next.

Epoxy Resin Furniture

From Maker Trend to Mainstream Category

Epoxy resin furniture built its early audience through small-batch makers and social media — river tables and live-edge slabs went viral well before big retailers took the category seriously. That phase isn’t over, but it’s no longer the whole story. Mid-size furniture brands, and even some larger retailers, now carry resin pieces as a standard SKU rather than a novelty item.

What that shift means for sourcing: buyers further down this chain — brands, retailers, distributors — increasingly expect the same consistency and documentation from an epoxy resin manufacturer that they’d expect from any other furniture material supplier. Reliable batch-to-batch clarity, documented UV stability, and a manufacturer who can actually explain their formulation rather than just sell a drum of resin.

Live-Edge and River Tables: Still Strong, But Maturing

River tables and live-edge resin furniture remain the anchor of the category, and demand hasn’t meaningfully softened heading into 2026. What’s changed is buyer sophistication. Early buyers were often drawn purely by visual novelty. Today’s buyers — especially at the higher end — ask more pointed questions: is the resin UV-stable, what’s the expected yellowing timeline, is the piece food-safe if it’s a dining table, what’s the warranty.

That shift rewards suppliers and brands who can speak specifically to formulation, not just aesthetics. A furniture brand that can tell a customer their tabletop uses a non-yellowing, UV-stabilized deep pour epoxy — and back it up with a real technical data sheet — has a genuine edge over a competitor selling on photos alone.

Color and Pigment Trends Moving Into 2026

A few directional shifts are worth tracking for anyone formulating or stocking pigmented resin for furniture:

  • Earth tones and translucent naturals are gaining ground over the high-saturation “ocean blue” river table look that dominated the category’s early years. Sandy neutrals, smoky grays, and translucent ambers show up more often in higher-end furniture lines now.
  • Metallic and mica-based effects keep growing, particularly in smaller decorative and accent pieces — side tables, coasters, wall art — where a striking finish matters more than large-format clarity.
  • Two-tone and layered pours — distinct color bands or gradients within a single piece — turn up increasingly in mid-to-premium furniture, which calls for a resin system with a working time long enough to layer cleanly without the bands bleeding into one another.

For manufacturers and private label brands, this points toward demand for pigment systems and resin formulations flexible enough to support layered, multi-pour work — not just single-color casting.

Sustainability Questions Are Getting Louder

Sustainability hasn’t reshaped Epoxy Resin Furniture the way it’s reshaped apparel or packaging, but the questions keep getting more common — especially from younger buyers, and from retailers building out “responsibly sourced” product lines.

The honest picture: most epoxy resin is still petroleum-derived, and bio-based epoxy systems remain a smaller, pricier segment of the market rather than the mainstream. What’s shifting faster is transparency. Buyers and retailers increasingly want to know what’s actually in the resin — VOC content, any bio-based percentage, end-of-life considerations — rather than vague “eco-friendly” claims with nothing behind them.

For manufacturers, this is less about reformulating everything around a sustainability angle and more about answering specific composition questions honestly when a retail buyer asks, because more of them are starting to.

Wholesale and Private Label Demand Is Growing Faster Than DIY

The DIY and small-maker segment isn’t shrinking, but the growth curve in North America increasingly comes from the wholesale and private label side — furniture brands and distributors sourcing finished or semi-finished resin furniture and resin-topped pieces at volume, rather than individual makers buying a pail of resin for one project.

A few practical signals show up for anyone sourcing right now:

  • Buyers ask for consistent batch clarity across large orders, not just a good-looking single sample.
  • Private label and OEM inquiries for furniture-grade epoxy keep climbing, as furniture brands look to build resin pieces into a standard product line rather than a limited drop.
  • Lead time and capacity questions surface earlier in sourcing conversations, since a furniture brand planning a retail launch needs supply reliability a hobbyist buyer never had to think about.

Regional Notes: US, Canada, and Cross-Border Sourcing

The US remains the largest market in the region by a wide margin, with the strongest concentration of demand in home furnishings, hospitality (restaurant and bar tabletops especially), and custom residential builds. Canada’s market is smaller but growing, with a similar aesthetic profile to the US and comparable appetite for live-edge and river table pieces, particularly in custom and small-batch furniture segments.

For manufacturers and distributors selling across both markets, the practical differences are mostly regulatory rather than aesthetic. Labeling and compliance requirements aren’t identical between the US and Canada, so a supplier serving both needs documentation covering both markets rather than assuming one label fits everywhere.

What This Means If You’re Sourcing in 2026

A few practical takeaways for buyers navigating the Epoxy Resin Furniture category through the rest of the year:

  1. Ask for real technical documentation, not just photos. UV stability, yellowing data, and food-safety documentation for dining and kitchen pieces are increasingly expected by end buyers, so get this from your manufacturer before your own customers start asking.
  2. Prioritize formulation flexibility if you’re doing layered or multi-tone work. A resin system with a longer, more controllable working time supports the layered and two-tone pours gaining ground in the category.
  3. Get specific on composition if sustainability comes up. Vague claims don’t hold up under buyer scrutiny anymore — know what’s actually in your resin.
  4. If you’re scaling from small-batch to wholesale, talk to your manufacturer about capacity early. Consistency across a large order is a different production challenge than a single showcase piece, and it’s worth confirming your supplier can actually deliver at the volume you’re planning to sell.

Frequently Asked Questions

Is epoxy resin furniture still trending in 2026? Yes — demand has matured rather than peaked. Growth is shifting from individual maker sales toward wholesale and private label furniture brands building resin pieces into standard product lines.

What resin colors are most popular for furniture right now? Earth tones, translucent neutrals, and metallic or mica-based accents are gaining ground alongside the classic ocean-blue river table look, particularly in higher-end furniture lines.

Is epoxy resin furniture sustainable? Most epoxy resin is still petroleum-derived. Bio-based options exist but remain a smaller, pricier segment. Buyers care more about transparency around actual composition right now than sustainability marketing claims.

What should furniture brands ask an epoxy resin manufacturer before sourcing at volume? Ask about UV stability and yellowing data, food-safety documentation for dining pieces, batch-to-batch clarity consistency, and production capacity for scaling from sample runs to wholesale volume.

The Bottom Line

Epoxy Resin Furniture in North America isn’t a fading trend — it’s a category growing up. Sharper technical questions from buyers, the shift toward wholesale and private label demand, and rising expectations around documentation all point the same direction: suppliers and brands who can back their resin furniture with real data, not just good photography, are the ones best positioned heading through 2026.

Private Label Epoxy Resin

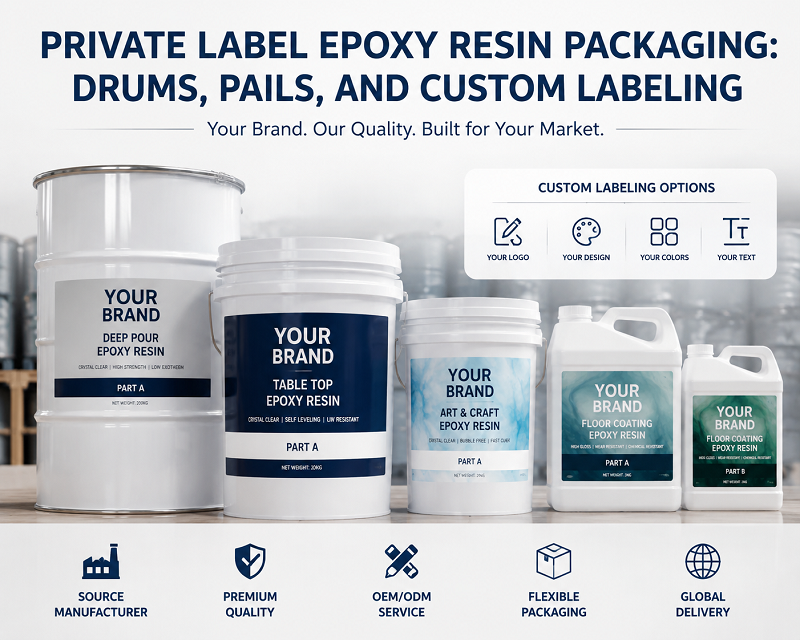
Private Label Epoxy Resin Packaging: Drums, Pails, and Custom Labeling

Most private label epoxy resin conversations start with formulation and price. Packaging tends to come up last — often once the formula is locked and the first production run is already on the calendar. That’s the wrong order to do it in. Epoxy Resin Packaging decisions affect your unit economics, your freight cost, and how your brand actually looks on a customer’s shelf or job site, so it’s worth sorting out before you finalize an order, not after.

Below is what an Epoxy Resin Manufacturer can typically offer on the packaging side, and what each option actually means once you’re the one placing the order.

Private Label Epoxy Resin

Standard Container Formats

Drums (200L / 55-gallon). The standard format for bulk industrial buyers — flooring contractors, large-volume distributors, manufacturers blending epoxy into their own downstream products. Drums keep per-liter packaging cost down and are the most freight-efficient choice for full-container orders. The catch is handling: drums need pumps or dispensing equipment on the receiving end, which makes them impractical for a brand selling straight to end consumers.

Pails (5-gallon / 20L and smaller). The format most brands selling table top epoxy and deep pour epoxy actually use when their buyers are makers, hobbyists, and small contractors. End users can handle pails without special equipment, and it’s the size most private label furniture and countertop brands put their logo on. Smaller pail sizes — 1 gallon, 1L, quart — exist too, usually reserved for sample kits, small craft projects, or premium retail lines.

Kits. Resin and hardener packaged together at matched, pre-measured ratios, often in a branded box with mixing instructions included. Retail-facing DIY and craft brands lean on this format because it removes the guesswork around mix ratio and cuts down on returns from buyers who get it wrong. Producing and packing a kit costs more per liter than bulk drums or pails, but for a consumer-facing brand, less support burden and a better shelf presence usually make up the difference.

What “Private Label Epoxy Resin” Actually Covers on the Packaging Side

Private label epoxy resin packaging isn’t one fixed service. Manufacturers typically offer a few different tiers, and it pays to be specific about which one you actually mean.

Neutral packaging with your label applied. The manufacturer’s standard container — drum, pail, or bottle — with your brand’s label or sticker applied before it ships. Fastest option, lowest MOQ, and usually where a new private label relationship starts.

Custom-printed packaging. Your logo and branding printed directly onto the container instead of applied as a sticker — silkscreened or printed pails, custom-printed kit boxes, branded caps. Looks noticeably more polished on a retail shelf, but the MOQ climbs, since the manufacturer has to run a dedicated print job rather than slap on stock labels.

Fully custom container design. A bottle, pail, or box shape built specifically for your brand, sometimes with dedicated molds. The highest-investment tier, generally reserved for brands already moving real volume — custom tooling carries upfront cost that only pencils out once order volume justifies it.

If you’re early-stage, starting with neutral packaging plus your own label is almost always the right call. It lets you test the market and build a sales history without committing to tooling or an MOQ tier you may not need yet.

Labeling Requirements Buyers Often Miss

Private label epoxy resin orders most often stall here — not because the manufacturer got something wrong, but because the label content wasn’t finalized before production started.

Hazard labeling (GHS). Epoxy resin and hardener components typically need GHS hazard pictograms, signal words, and hazard statements on the label, pulled directly from the SDS. This isn’t discretionary branding space. It’s a regulatory requirement in most export markets, and it has to match your specific formulation — not a generic template pulled from somewhere else.

Country-specific requirements. The US, EU, UK, and Australia don’t all require identical label content or formatting. Selling into more than one of these markets means confirming with your manufacturer, or your own compliance resource, whether a single label design covers all of them or whether you need market-specific versions.

Net content and mix ratio. Anyone assembling a kit brand needs this printed clearly for the end user, especially when resin and hardener aren’t a clean 1:1 ratio. A mismatched or unclear label here is one of the most common sources of end-user mixing errors — and the support complaints that follow.

Batch and lot numbers. Useful for your own quality tracking, and often expected by your own B2B customers who need traceability on their end. Worth confirming whether your manufacturer can print or apply these per production run, and exactly where on the label they’ll show up.

Get the label content — hazard statements, net content, mix ratio, batch numbering — finalized and signed off before your manufacturer schedules the run. A label revision after production starts is one of the more common, and more avoidable, causes of delay on private label orders.

Freight and MOQ Implications by Format

Packaging format moves your freight math more than most first-time buyers expect.

Drums stack efficiently and maximize how much volume fits per container, which is the standard reason large-volume buyers default to them — lower per-liter freight cost. Pails and kits take up more space relative to the actual resin inside, since you’re shipping packaging as well as product, which pushes per-unit freight cost up.

MOQ generally scales with how customized the packaging is. Neutral labeled pails tend to carry a relatively low MOQ, custom-printed packaging sits higher, and fully custom container tooling sits at the top, since the manufacturer needs a large enough run to recoup setup cost. If your current volume doesn’t clear a higher MOQ tier yet, ask your Epoxy Resin Manufacturer directly what applies at each packaging level rather than guessing — sometimes the gap between tiers is smaller than buyers assume, sometimes it’s considerably larger.

Questions Worth Asking Before You Commit

Short list, but each one can shift your cost, your timeline, or your compliance exposure:

  1. What packaging formats do you offer as standard, and what’s the MOQ at each?
  2. Can you apply GHS-compliant labels for our target export markets, or do we need to supply compliant label artwork ourselves?
  3. What’s the lead time difference between neutral labeling and custom-printed packaging?
  4. Can batch or lot numbers be printed or applied per production run?
  5. If we outgrow pails and move to drums — or the other way around — how does that change pricing and MOQ?

The Bottom Line

Packaging isn’t a cosmetic add-on to a private label epoxy resin order. It’s a decision that touches your freight cost, your compliance obligations, and how your brand actually shows up in front of the person using the product. Get specific with your Epoxy Resin Manufacturer about format, labeling requirements, and MOQ at each customization tier before the formula gets finalized — not after.

Epoxy Resin Manufacturer (7)

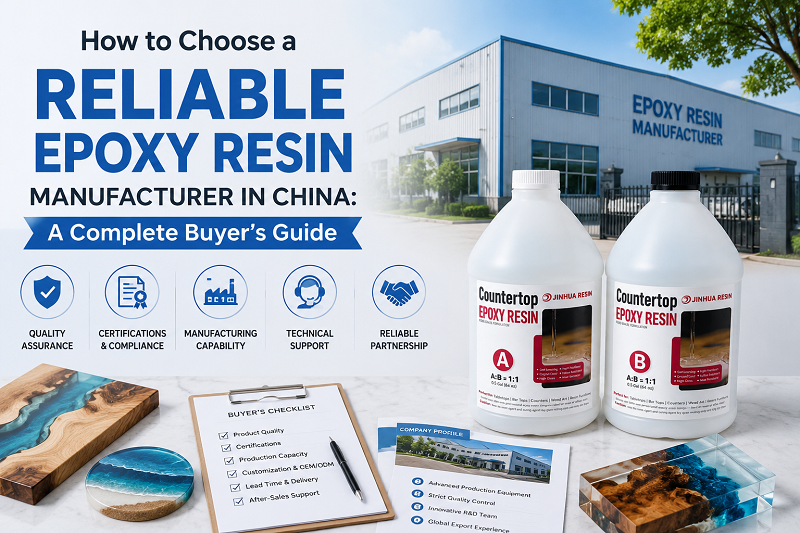
How to Choose a Reliable Epoxy Resin Manufacturer in China: A Complete Buyer’s Guide

Introduction

Anyone can find an epoxy resin supplier in China with a quick search. The hard part comes later — after you’ve placed a real order for a few thousand kilograms and need the tenth batch to match the first.

Here’s the pattern most buyers run into: the sample is flawless. Clear, well-cured, exactly what they asked for. Then production scales up, and suddenly viscosity drifts, cure times shift, or the packaging that showed up doesn’t match what was agreed on.

Picking an Epoxy Resin Manufacturer isn’t a line item on a purchasing spreadsheet. It’s a bet on whether your product line still looks the same a year from now. China’s epoxy resin industry has grown deep enough to serve woodworking, furniture, crafts, flooring, construction, and private-label lines — but depth of options doesn’t make the selection process any easier. It just raises the number of ways to get it wrong.

Epoxy Resin Manufacturer (7)

1. A Supplier Sells You Product. A Manufacturer Controls the Process.

That distinction matters more than most buyers realize going in.

Work with a trading company and you’re often buying blind on:

  • How the resin is actually produced
  • Who controls the formula, and how tightly
  • What the inspection process looks like — if there is one
  • Real production capacity, not the number on a brochure

A factory that runs its own process, from raw material sourcing to final packaging, can answer those questions directly. No middleman guessing on your behalf.

Take river tables as an example. Buyers need deep pour epoxy with low viscosity, strong clarity, a long working window, and heat release that won’t crack the pour. None of that happens by accident — it comes from a factory that’s solved those problems before, repeatedly.

2. What Buyers Who’ve Been Burned Before Actually Check

Ask anyone who’s imported epoxy resin more than once, and they’ll tell you the checklist gets shorter and more specific over time.

Does the factory actually own its production floor? This is step one. A rented name on a listing isn’t the same as owned equipment.

Can they handle both R&D samples and repeat bulk runs? Some shops are built for one-off custom batches. Others can do that and then reproduce it at scale — that’s a different capability.

Is there a real inspection process, or just a claim of one? Consistency isn’t a promise — it’s a documented step-by-step check.

Do they understand export paperwork? Documentation, compliant packaging, and communication that doesn’t require three follow-up emails per question — all signs of a manufacturer used to shipping overseas.

3. The First Sample Tells You Almost Nothing

A strong first sample proves the factory can make epoxy resin once. It says nothing about batch five, fifty, or five hundred.

Where production control breaks down, you’ll typically see:

  • Viscosity shifting batch to batch
  • Cure performance that’s inconsistent under the same conditions
  • Color drift
  • Surface finish that changes without explanation

A manufacturer worth working with treats repeatability as the actual product — not the sample that got you to sign.

4. Formula Development Is Where the Real Value Sits

Different end markets need genuinely different resin chemistry, not a relabeled version of the same product.

Deep Pour Epoxy buyers typically need:

  • Low viscosity for clean pours
  • High transparency
  • A long curing window
  • Controlled exothermic reaction

Table Top Epoxy buyers care more about:

  • A smooth, self-leveling finish
  • High gloss
  • Surface durability

UV Resin buyers want:

  • Fast cure under UV light
  • Optical clarity
  • Simple, forgiving application

Industrial floor coating buyers prioritize:

  • Long-term wear resistance
  • Chemical resistance
  • Adhesion that holds under load

A manufacturer with real formula development capability builds toward what you need. One without it just sells you what’s already on the shelf.

5. OEM and Private Label — Where China Manufacturing Actually Pays Off

For overseas brands, OEM capability is often the single deciding factor in choosing a Chinese partner over a local one.

A manufacturer that does OEM well typically offers:

  • Formula tuning for your specific application
  • Product customization beyond color and viscosity
  • Branded packaging
  • Label design support
  • Technical documentation ready for your market
  • Formulations adjusted for regional regulations or climate

The right partner doesn’t hand you their catalog and call it private label. They help build something that fits your customer base specifically.

6. Mistakes Buyers Keep Making — Even Experienced Ones

Buying on price alone. The lowest quote is rarely the lowest total cost once quality issues show up mid-production.

Skipping the technical documents. TDS, SDS/MSDS, and COA aren’t paperwork for paperwork’s sake — they tell you what you’re actually buying.

Skipping application testing. A sample that looks fine on a lab bench can behave differently in your actual use case. Test it there.

Not asking about future capacity. If your order volume doubles next year, can this factory scale with you — or are you starting the search over?

7. What Quality Control Looks Like Inside a Real Epoxy Resin Factory

A production process built for consistency generally runs through:

Raw material inspection → Formula preparation → Mixing control → Performance testing → Packaging inspection → Final quality approval

Skip any one of those steps and batch-to-batch consistency becomes a matter of luck rather than process.

8. Why Buyers Keep Coming Back to Jinhua Resin

Jinhua Resin builds custom resin solutions for buyers across global markets — as a manufacturer, not a reseller.

The process starts with understanding what you’re actually trying to build:

Inquiry → Application analysis → Sample testing → Formula adjustment → Trial order → Mass production

Product lines include:

  • Deep Pour Epoxy Resin
  • Table Top Epoxy Resin
  • UV Resin
  • Epoxy Floor Coating
  • Crystal Clear Epoxy Resin
  • Casting Epoxy Resin
  • Custom Formula Epoxy Resin
  • Private Label Epoxy Resin

Distributor, brand owner, or industrial buyer — the manufacturing support and formula customization scale to what your business actually needs.

FAQ

Q1: How do I choose an epoxy resin manufacturer in China? Look at factory ownership, quality control process, technical support, export track record, and how far their customization actually goes.

Q2: What should I check before importing epoxy resin? Samples tested in your real application, complete technical documents, verified production capacity, packaging options, and how long they’ve actually been exporting.

Q3: Can epoxy resin manufacturers customize products? The capable ones can adjust formula, viscosity, cure speed, color, and packaging — not just relabel a standard product.

Q4: What documents should suppliers provide? At minimum: TDS, SDS/MSDS, and COA.

Q5: What’s the real difference between a factory and a trading company? A factory controls the formula, the process, and the quality checks directly. A trading company is sourcing from someone else and passing it along.

Epoxy Resin Flooring Vs. Countertop Grade

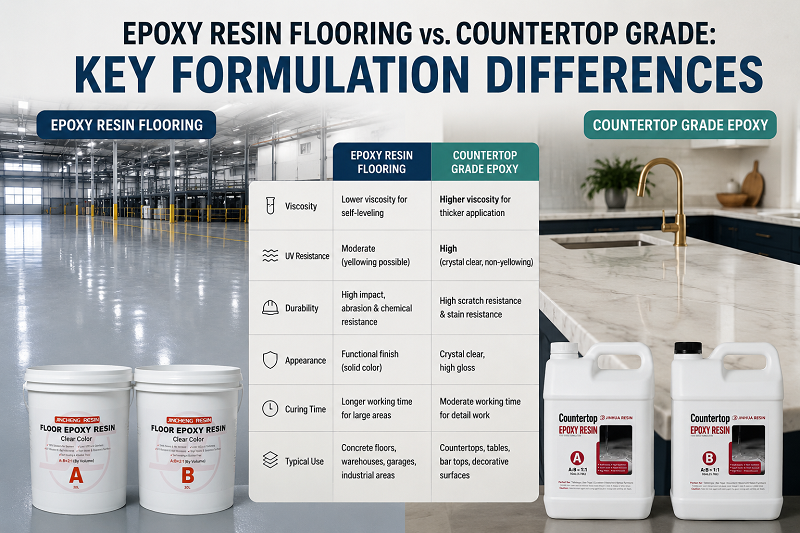
Epoxy Resin Flooring vs. Countertop Grade: Key Formulation Differences

“Can I just use the same epoxy for my floor and my countertop?” We get this question more often than you’d think — usually from a distributor trying to simplify their catalog, or a first-time buyer hoping to avoid stacking MOQs across two product lines.

Short answer: no. Not if you want either surface to actually perform. Epoxy Resin Floor Coating and countertop epoxy start from different design briefs, and that shows up in nearly every property that matters — viscosity, hardness, UV stability, cure speed, even what gets mixed in. Below is where the two genuinely diverge, and why a manufacturer formulates them as separate product lines in the first place rather than one “universal” epoxy.

Epoxy Resin Flooring Vs. Countertop Grade

Different Jobs, Different Priorities

A countertop sits indoors, gets wiped down daily, and is expected to stay glass-clear for years. It needs to shrug off knife nicks, tolerate a hot pan set down without thinking, and hold its clarity under UV coming through a kitchen window.

A floor gets walked on, rolled over with carts, hit with spills and chemicals, and in industrial or garage settings, ground down by tire traffic and foot traffic all day. Clarity almost never matters here. What matters is impact resistance, chemical resistance, and slip resistance.

Those two very different jobs are the reason the resin systems split apart from the first stage of formulation — not a marketing distinction, a chemistry one.

Viscosity and Application Method

Countertop-grade resin is generally built to self-level: low enough viscosity to spread into a smooth, glass-like surface, but controlled enough that it doesn’t run off the edge of a mold before it starts to gel.

Flooring formulations vary more, because floors get applied differently depending on the job:

  • Self-leveling floor epoxy sits at a viscosity close to countertop resin — used for seamless, high-gloss commercial and residential floors.
  • Trowel-applied or broadcast systems run thicker, often loaded with aggregate (silica sand, quartz) to build texture and thickness for industrial or garage floors that need real mechanical toughness.
  • Mortar and screed systems, the thickest tier, are almost paste-like — mixed with graded sand for warehouses and production floors expected to take heavy, repeated loads.

Pour a countertop-grade resin at trowel thickness on a floor, and it probably won’t self-level the way you’d want, may trap air it wasn’t designed to release, and won’t hold up to abrasion the way a floor needs. Do the reverse — flooring epoxy poured at countertop thickness on a tabletop — and you risk fast, uneven cure, more trapped bubbles, or a finish that never reaches the water-clear look buyers expect from Table Top Epoxy Resin.

UV Stability: The Biggest Chemistry Split

This is where the two categories part ways most sharply at the molecular level.

Countertop and table top epoxy resins almost always carry UV stabilizers, often built on non-yellowing chemistry — aliphatic hardener systems, or hybrid blends — because yellowing is one of the most visible, most complained-about defects in clear cast work. A countertop that starts yellowing six months after installation, sitting under a kitchen window, is a warranty claim in the making.

Epoxy Resin Floor Coating, especially base coats and industrial systems, typically runs on standard — often aromatic — resin chemistry, which yellows faster under UV. For flooring, that trade-off is usually fine. Most commercial and industrial floors either stay out of direct sun or get finished with a UV-stable polyurethane or polyaspartic topcoat specifically to handle sun exposure and add abrasion resistance. The epoxy base coat doesn’t need to be UV-stable on its own; the topcoat is doing that job.

Buyers who source flooring epoxy purely for yellowing resistance — without realizing a topcoat system is standard practice — sometimes end up paying for UV stability they don’t need, or worse, skipping the topcoat they actually do.

Hardness and Wear Resistance

Both categories cure hard. But “hard” means something different depending on what the surface has to survive.

Countertop epoxy targets scratch and mar resistance suited to kitchen use — knife nicks, a hot pan within stated limits, daily wiping with cleaning products.

Flooring epoxy, industrial-grade especially, is built for a different kind of durability: compressive strength and abrasion resistance under sustained mechanical load — forklifts, dropped tools, rolling equipment, years of impact rather than months. That usually calls for a higher cross-link density formulation, sometimes combined with aggregate fillers doing mechanical work the resin can’t do alone.

Shore D hardness numbers can look nearly identical between a countertop product and a flooring product on paper. But hardness alone says little about abrasion or impact resistance — the two properties that actually matter most for a floor.

Chemical and Stain Resistance

Both are epoxy systems, so both hold up reasonably well against chemicals compared with other coatings — but what they’re tested against differs.

Countertop epoxy is generally tested and marketed against household stains: wine, coffee, cooking oil, mild kitchen acids. Flooring epoxy, particularly industrial and commercial grades, is tested against a rougher list — motor oil, solvents, cleaning chemicals, sometimes battery acid or facility-specific chemicals. A formulation built for an auto shop floor is solving a different chemical-resistance problem than one built for a kitchen countertop, even though both get labeled “epoxy resin” on the box.

Additives: What Actually Goes Into Each System

This might be the clearest way to tell the two categories apart — just look at what’s in the mix.

Countertop and Table Top Epoxy Resin typically include:

  • UV stabilizers and non-yellowing agents
  • Defoamers, for a bubble-free clear finish
  • Pigments or dyes for color work — or nothing at all, for water-clear casting
  • Occasionally mica powders or metallic pigments for decorative pours

Epoxy Resin Floor Coating typically includes:

  • Aggregate fillers — silica sand, quartz — for texture, slip resistance, and buildable thickness
  • Color flake or chip blends for commercial and garage floor finishes
  • Anti-slip additives for safety compliance in wet or industrial spaces
  • Occasionally conductive or static-dissipative additives for specialized industrial floors, like electronics manufacturing

If you’re vetting a supplier’s private label capability, this is worth asking directly: does their formulation team actually work across both additive categories, or does production really specialize in one? Floor systems bring their own set of formulation and application questions that a countertop-focused supplier may not be set up to answer.

Cure Profile and Pot Life

Countertop resin is usually formulated with a longer working time, giving room for detailed pours, embedded objects, and multi-layer work without the material gelling mid-project. Full cure on a clear cast countertop can take several days to reach full hardness and chemical resistance, even if it’s touch-dry within 24 hours.

Flooring systems, especially in commercial settings where downtime costs money, are often formulated to get back into service faster — reopening to foot or vehicle traffic within 24 to 72 hours is common. That typically means a different hardener chemistry and a faster cross-link speed than a countertop system, which prioritizes working time over turnaround.

Cost and MOQ Considerations for Buyers

This is where the formulation gap turns into a purchasing decision.

Countertop-grade and UV-stable formulations generally cost more per kilogram than standard Epoxy Resin Floor Coating base coat, mostly due to the UV stabilizer package and the tighter quality control a clear, bubble-free finish demands. If you’re a distributor stocking both categories, don’t assume one blended MOQ or price tier covers your whole catalog — ask for separate technical data sheets and separate pricing per grade.

If your business sells into both flooring and furniture/countertop markets — common among private label distributors — it’s worth confirming early whether your manufacturer can reliably formulate and supply both grades, or whether they really specialize in one. A supplier strong in deep pour epoxy for tabletops isn’t automatically equipped for an industrial, aggregate-loaded flooring system. The reverse is just as true.

The Bottom Line

Epoxy Resin Floor Coating and Table Top Epoxy Resin share a resin chemistry family, but they’re engineered around different problems. Countertop formulations chase clarity, UV stability, and a self-leveling finish. Flooring formulations chase abrasion resistance, mechanical durability, and flexibility across trowel, broadcast, and self-leveling application methods.

Before placing an order — especially a private label or OEM order — confirm which grade you actually need, and get data specific to that grade from your manufacturer. The wrong grade in the wrong place doesn’t just underperform. It fails in ways that get expensive to fix after the fact.

Epoxy Resin Manufacturer

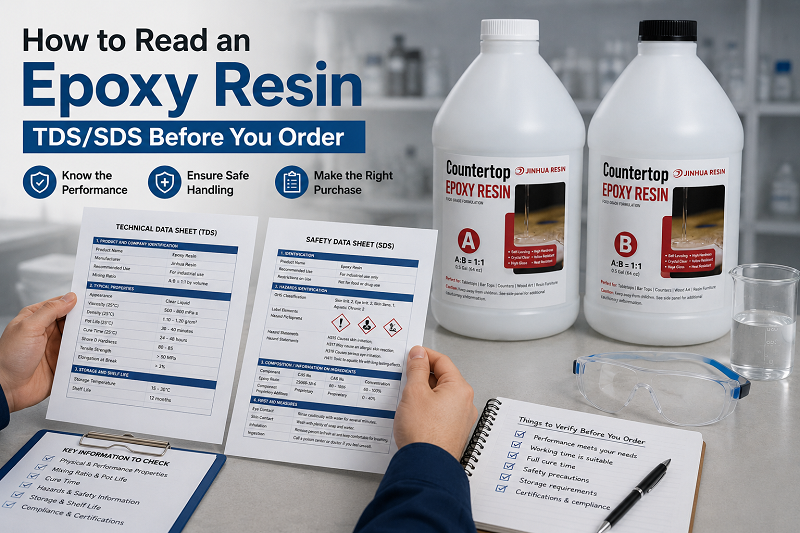
How to Read an Epoxy Resin TDS/SDS Before You Order

Ask ten buyers what they check before placing an order and most will say price, then lead time. The data sheets usually come third, if at all. That’s the wrong order. A TDS and SDS will tell you more about whether a supplier can actually hold to spec than a sales call ever will.

TDS vs. SDS — they’re not the same document

A Technical Data Sheet covers performance: viscosity, mix ratio, pot life, cure time, hardness, clarity. It’s the “what this resin does” document.

A Safety Data Sheet covers composition and hazard: chemical makeup, handling rules, exposure limits, disposal requirements. It’s the “what this resin is” document.

A lot of buyers sourcing from an epoxy resin manufacturer file both away without reading them closely. Worth changing that habit. These two sheets are often the fastest way to catch a mismatch before it turns into a production problem three months later.

Epoxy Resin Manufacturer

What to look at on the TDS first

Start with the mix ratio. Check whether it’s given by volume, by weight, or both. A supplier who lists only one number is handing you half the picture — resin and hardener rarely share the same density, so the volume ratio and the weight ratio diverge. Dose by the wrong figure and the cure chemistry drifts off.

Then pot life and cure time. People mix these up constantly, and honestly some suppliers do too. Pot life is how long the mixed batch stays workable once you’ve combined resin and hardener. Cure time is how long it takes to fully harden once poured or applied. A 45-minute pot life paired with a 24-hour cure behaves nothing like a 20-minute pot life paired with a 72-hour cure, even if both products get marketed under the same “deep pour epoxy” label.

Viscosity is next, and the number means little without a temperature attached. A resin rated at 400 cP at 25°C could run closer to 800 cP in a workshop that sits at 15°C in winter. If your production floor runs cold, ask the supplier for viscosity figures at your actual working temperature — the lab standard alone won’t tell you much.

For deep pour specifically, check the maximum pour depth listed. Go past it and you risk exothermic cracking, cloudiness, or yellowing — defects that only show up after the resin has cured, at which point there’s no fixing them. If a TDS skips this figure entirely, ask before you order, not after.

And for table top epoxy, look at Shore hardness and any notes on UV stability or long-term yellowing. A resin that scratches within weeks or ambers within a season generates returns. Not repeat business.

What to look at on the SDS first

Section 3 lists the chemical composition and CAS numbers. If you sell into a regulated market, this is the section your compliance team will actually pull from — not whatever’s on the product landing page.

Section 9 has flash point, VOC content, specific gravity. These figures drive shipping classification and storage rules, which affect landed cost more than most buyers expect going in.

Section 15 covers regulatory declarations — REACH, RoHS, and similar. If a supplier can’t produce an SDS with this section properly filled out, that’s not automatically a dealbreaker, but it’s reason enough to ask more before committing to volume.

Signs worth pausing on

A generic SDS that doesn’t quite match the product you ordered. Some manufacturers run one template SDS across an entire resin line, which means the hazard data on file may not reflect what’s actually in your specific batch.

No batch-to-batch tolerance data on the TDS. Ask directly what variance the manufacturer holds on viscosity and pot life run to run. Plus or minus 5% is normal. A supplier who can’t answer that question at all is telling you something, even without meaning to.

Numbers with no test method behind them. A data sheet worth trusting cites the standard for each figure it reports — ASTM D2196 for viscosity, ASTM D2240 for hardness, and so on. Figures without a method are harder to verify, and harder to hold anyone accountable to later.

Why this is worth the extra ten minutes

These two documents aren’t paperwork you glance at once and file. Read closely, they’re the clearest signal available before you place an order — whether this manufacturer actually controls their process, or is reselling whatever came off the line that particular week.

A supplier worth ordering from should answer follow-up questions on both sheets without hedging, and should be willing to test at your real working conditions rather than pointing back to lab standard numbers. If they can’t, that tells you plenty on its own.

Epoxy Resin Manufacturers (3)

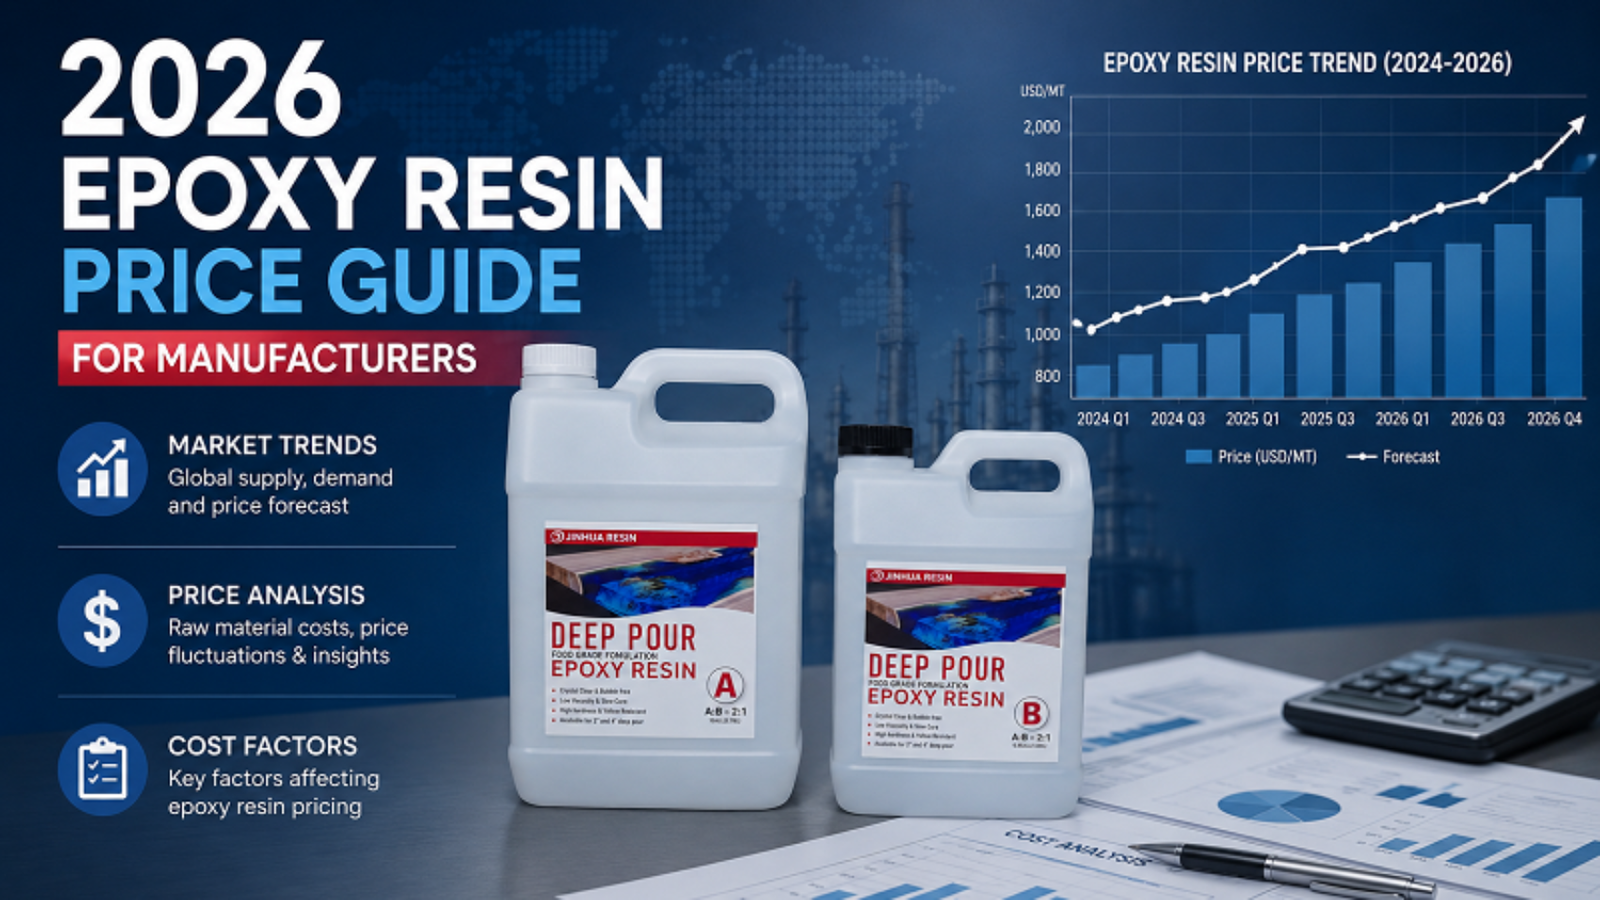
2026 Epoxy Resin Price Guide for Manufacturers

If you’ve been sourcing epoxy resin for any length of time, you already know that “stable pricing” is more of an aspiration than a guarantee. But 2026 has been a particularly sharp reminder of that reality — and for procurement teams and epoxy resin manufacturers alike, understanding what’s driving current prices isn’t optional anymore. It’s operational.

This guide breaks down where prices actually stand, what’s been pushing them around, and what to watch going into the second half of the year.

Epoxy Resin Manufacturers (3)

Where Prices Stand Right Now

Regional price gaps in 2026 are wider than most buyers budgeted for. Here’s the rough picture as of Q1–Q2:

  • Northeast Asia: ~$2.62/kg
  • Southeast Asia: ~$3.10/kg
  • Middle East: up 31.9% since late 2025, driven by feedstock tightening
  • Europe: ~$5.23/kg — the steepest in the major markets

For any epoxy resin manufacturer operating across multiple regions, these aren’t just numbers to track — they’re decisions waiting to happen. Whether you’re locking in contracts, adjusting formulas, or rethinking sourcing geography, the spread matters.


What’s Actually Moving the Market

Prices don’t shift in a vacuum. In 2026, several overlapping forces have been doing the heavy lifting:

Feedstock Pressure at the Top
Bisphenol A (BPA) and Epichlorohydrin (ECH) — the two primary raw inputs for most epoxy systems — saw sustained cost increases through late 2025 and into early 2026. When your inputs get more expensive and supply doesn’t loosen up, the pressure flows downstream quickly. Every epoxy resin manufacturer felt this, but how much of it reached the end buyer depended almost entirely on how well-positioned their procurement was heading into the year.

Geopolitical Friction and Shipping Disruption
Conflict-related disruptions in key trade corridors pushed freight costs up and complicated lead times. For epoxy resin manufacturers running lean inventory models, this created a compounding problem — higher input costs plus longer replenishment cycles meant tighter margins and less pricing flexibility.

Demand Spikes in High-Growth Sectors
The electric vehicle and renewable energy buildout hasn’t slowed down. Both sectors are heavy consumers of epoxy-based materials — battery encapsulation, structural composites, wind blade manufacturing. That demand pull has kept the market tight even when supply conditions might otherwise have allowed some relief.

Asian Supply Tightening
Scheduled maintenance shutdowns and capacity adjustments among major Asian producers created temporary but significant supply gaps, particularly in Q1. For buyers who rely heavily on a single sourcing region, this was a painful quarter.


How Smart Manufacturers Are Responding

Not every epoxy resin manufacturer navigated 2026 the same way. The ones that came through with minimal disruption tended to share a few common approaches:

They bought ahead, not behind.
Forward procurement — building inventory when feedstock prices dipped — gave some manufacturers a meaningful cost cushion that competitors without that buffer simply didn’t have. It’s not a complicated strategy, but it requires discipline and market visibility to execute consistently.

They diversified their supplier base.
Relying on a single BPA or ECH supplier in a tight market is a structural vulnerability. The epoxy resin manufacturers that fared best in Q1 were the ones that had already spread their upstream dependencies across multiple partners and geographies.

They locked in contracts where it made sense.
Spot buying can look attractive when prices are falling. In a rising market, it’s a liability. Manufacturers with long-term supply agreements in place were insulated — at least partially — from the worst of the Q1 run-up.

They communicated early.
This one doesn’t show up in a cost model, but it matters: manufacturers that flagged potential price or lead time impacts to their customers weeks in advance — rather than days — preserved relationships that spot-buying situations tend to fracture.


What to Watch in H2 2026

The back half of the year brings its own set of variables. A few things worth tracking closely:

BPA and ECH feedstock trajectory. If upstream costs stabilize, there’s room for some regional price softening — particularly in Asia. If they don’t, the pressure stays.

EV and renewable energy demand. Order books in both sectors remain strong. Unless that changes materially, demand-side pressure on epoxy resin isn’t going anywhere.

Regional capacity additions. Several new production facilities are expected to come online in Asia through 2026 and 2027. If timelines hold, this could shift the supply picture meaningfully by late Q4.

Currency and freight. Dollar strength and ongoing freight volatility continue to affect landed costs for buyers sourcing internationally — something every epoxy resin manufacturer with a cross-border supply chain needs to factor in.


A Note on What Price Guides Don’t Tell You

Spot prices and regional averages are useful benchmarks, but they don’t capture the full picture of what you’re actually paying — or what you’re risking.

The epoxy resin manufacturer quoting you the lowest price today might be doing so because they haven’t yet passed on their own cost increases. That gap closes eventually, sometimes suddenly. The one quoting slightly higher might be the one whose supply chain is actually in a position to deliver reliably six months from now.

Price is one input into a sourcing decision. Supply continuity, relationship depth, and the ability to absorb market shocks without disrupting your production schedule are the variables that tend to matter more when things get difficult — which, based on 2026 so far, is a scenario worth planning for.


Bottom Line

2026 has been a year that separated well-structured epoxy resin manufacturers from those operating on thinner foundations. The price volatility was real, but so was the variation in how different suppliers responded to it.

For buyers, the takeaway is straightforward: use this moment to pressure-test your current supplier relationships. For manufacturers, it’s a reminder that supply chain resilience isn’t a cost center — it’s a competitive advantage that shows up most clearly when the market stops cooperating.

Prices will settle. The habits built around managing through volatility tend to stick around longer.

Epoxy Resin Manufacturers (2)

River Tables and River Countertops: Why Furniture Brands Are Shifting to Deep Pour Epoxy Wholesale Sourcing

A Product Category That Outgrew Its DIY Origins

River tables started as a niche project in the custom woodworking community — live-edge slabs, deep-fill epoxy channels, conference tables that commanded five-figure prices from architects and interior designers. That was ten years ago. Today, river tables appear in furniture retail chains, hospitality fit-outs, residential kitchen renovations, and mass-market home goods catalogues. The aesthetic went mainstream. The supply chain didn’t keep up.

Most of the deep pour epoxy resin reaching North American and Australian furniture makers still moves through the same fragmented channels it did when river tables were a hobbyist pursuit: craft supply distributors, small-batch resin brands, direct import by individual studios. For B2B buyers — furniture brands, wholesale distributors, contract manufacturers — the opportunity is in professionalization: bringing supply chain discipline, consistent formulation quality, and volume pricing to a segment that has mostly operated without it.

This article maps the B2B demand structure for deep pour epoxy in the furniture market, explains why formulation requirements for professional furniture applications differ from hobbyist products, and identifies what wholesale buyers should look for when qualifying a Chinese epoxy resin manufacturer for this segment.

Epoxy Resin Manufacturers (2)

The Market Structure: Who’s Actually Buying Deep Pour Epoxy

Understanding the demand structure matters for anyone building a wholesale or distribution business in this space. Deep pour epoxy buyers in the furniture sector aren’t a monolithic customer base — they have different volume requirements, different formulation needs, and different purchasing behaviors.

Custom Furniture Studios

Single-operator or small-team workshops producing bespoke river tables, live-edge dining tables, and custom bar tops. Volume per order: 5–50 liters. Purchasing frequency: irregular, project-driven. Price sensitivity: moderate — they’re selling finished pieces at significant markup and can absorb a premium for product they trust. What they care about most: optical clarity, color stability (their finished pieces need to look the same in five years as they do on delivery), and reliable technical support when something goes wrong.

This is the buyer who reads every line of a TDS and calls the supplier when the pour behaves differently from last time. For distributors, they’re high-touch but high-loyalty. Get the product right and they don’t switch.

Mid-Scale Production Furniture Brands

Companies producing river table collections for retail — furniture stores, online platforms, hospitality procurement channels. Volume per order: 100–500 liters. Purchasing frequency: monthly or quarterly. Price sensitivity: higher — they’re competing on price at the retail level and need consistent material cost. What they care about most: batch-to-batch consistency (finish quality needs to be identical across a production run of 50 tables), pour depth predictability, and documentation that supports their quality system.

This is the buyer who needs a Certificate of Analysis with every shipment and will run incoming inspection on resin properties. Supply disruption is a production line problem, not an inconvenience.

Contract Manufacturers and Hospitality Fit-Out Specialists

Companies pouring large-format epoxy elements — bar tops, reception counters, feature walls — for commercial clients. Volume per order: 200–2,000 liters. Purchasing frequency: project-based with occasional blanket orders. What they care about most: maximum pour depth per layer (commercial projects often require sections that exceed consumer product specifications), open time in large-volume pours, color match stability across multiple orders placed months apart.

This segment is the most technically demanding. The pour depth requirements push against the thermal management limits of most commercial deep pour products. Color consistency across orders requires a supplier with documented raw material stability, not just batch-to-batch QC.

Retail Resin Brands (Private Label)

Brands that source epoxy resin from China and sell under their own label — consumer packaging, branded documentation, positioned against retail competitors. Volume per order: 200–1,000 liters across multiple SKUs. What they care about: OEM capability, private label packaging, documentation that matches their brand’s quality positioning, and a supplier relationship that can scale with their growth.

This buyer is not buying a commodity. They’re buying a supply chain partnership. The epoxy resin manufacturer’s OEM capability — custom labeling, bilingual documentation, packaging format flexibility — is as important as the product specification.


Why Professional Furniture Applications Demand More Than Hobbyist Formulations

The deep pour epoxy products marketed to hobbyists and the formulations required for professional furniture production are not the same thing. The differences matter for B2B buyers who are supplying professional fabricators.

Pour Depth: The Commercial Reality

Consumer deep pour products are typically specified to a maximum single-layer depth of 50–75mm (2–3 inches). That covers most hobbyist applications. Commercial furniture production regularly requires deeper single pours — 100mm channels in wide river tables, 150mm decorative elements in hospitality installations, thick casting blocks for sculptural furniture components.

At these depths, the thermal management requirements are significantly more demanding. A product specified to 75mm maximum depth doesn’t just “work less well” at 100mm — it risks thermal runaway: exothermic overheating that causes cracking, yellowing, volatile release, and in severe cases, mold damage or fire. Professional fabricators working at commercial scale need products with documented pour depth limits above the 75mm consumer product ceiling, with supporting temperature rise data rather than marketing claims.

Color Consistency Across Production Runs

A custom furniture studio producing one table can manage minor color variation between the epoxy pours on that piece. A production furniture brand manufacturing 50 river tables for a retail order cannot — every table needs to be visually identical. A hospitality specifier ordering additional units of a feature counter six months after the initial installation cannot have a visible color shift between the original and the replacement.

Color consistency across production runs requires a supplier with documented raw material sourcing stability, batch-to-batch colorimetric testing, and a change control process that prevents undocumented formula adjustments. None of this is guaranteed by ISO 9001 alone — it has to be specifically verified.

Open Time in Large-Volume Pours

In commercial production environments, a single pour often involves mixing and placing significantly larger volumes than the 1–2 liter quantities typical of hobbyist application. Mixing 10 liters of deep pour epoxy generates more total exothermic heat than mixing 1 liter — even in a deep pour formulation. The effective pot life decreases as mixed volume increases, because the larger mass generates and retains more heat.

Professional buyers need pot life data across a range of mixed masses, not just the standard 100g or 150g laboratory test condition. A product with 60 minutes pot life at 150g may have 35 minutes effective pot life at 5,000g — a difference that matters significantly when managing a large commercial pour.

Ambient Temperature Performance Range

Consumer product documentation typically specifies performance at 20–25°C. Professional furniture production happens in workshops across diverse climate zones: a furniture factory in Queensland operates at ambient temperatures that routinely exceed 30°C in summer; a contract manufacturer in Minnesota works through winters where the shop floor drops below 15°C. Both conditions materially affect pot life, working time, and maximum pour depth.

Professional buyers sourcing deep pour epoxy for resale into diverse geographic markets need temperature-range data, not a single-condition specification.


The Wholesale Sourcing Equation: What Changes at Volume

Moving from sample purchases to wholesale supply relationships in the deep pour epoxy category changes the relevant evaluation criteria significantly.

Formulation Stability at Volume

At sample and small-order quantities, formulation variation between batches is masked by the fact that each order is typically used in a single pour session. At wholesale volumes — where a single shipment might supply a furniture brand for 8–12 weeks of production — batch-to-batch variation in viscosity, cure speed, or color accumulates and becomes visible in finished product output.

The QC regime required for wholesale supply is meaningfully more rigorous than for sample orders. Per-batch Certificate of Analysis is table stakes. What distinguishes serious wholesale suppliers from product sellers is the depth of that CoA: actual measured values (not pass/fail notation), colorimetric data (Gardner color or APHA), and viscosity data for both components at multiple temperatures.

Private Label Packaging for the Furniture Market

The furniture market has specific packaging conventions that differ from general-purpose resin applications. River table fabricators typically work in 1:1 or 2:1 ratio systems with component volumes matched for mixing convenience — a 15-liter Part A paired with a 7.5-liter Part B, for example, rather than arbitrary drum quantities that require customers to measure out matching weights.

Wholesale buyers supplying professional fabricators need a Chinese epoxy resin manufacturer capable of filling to matched-component specifications, not just bulk drums. Custom labels, application guides, and bilingual documentation (for markets like Canada with French-language requirements, or Australia with GHS-specific SDS format) are the basic OEM requirements for this channel.

Supply Consistency and Forward Planning

Professional furniture production can’t be managed around resin supply uncertainty. A furniture brand on a 6-week production cycle for a retail order needs to know that the epoxy supply will be available on schedule, with consistent specifications, for the duration of the order. Supply gaps, specification changes, or documentation delays at the manufacturer level translate directly into production delays and contract penalties at the furniture brand level.

Wholesale buyers should establish supply agreements that include volume commitments, lead time guarantees, advance notification of raw material changes, and defined remedies for supply failures. These provisions exist in mature industrial supply relationships — they’re not standard in the casual supplier-buyer conversations that characterize much of the deep pour epoxy market today.


Qualifying a Chinese Deep Pour Epoxy Manufacturer for Furniture Applications

The qualification criteria for a deep pour epoxy supplier serving professional furniture applications are more demanding than for general-purpose resin sourcing. These are the minimum requirements.

Pour depth documentation. Temperature rise curves at 50mm, 75mm, 100mm, and 150mm pour depths. Maximum recommended depth per layer at 20°C, 25°C, and 30°C ambient. This data should be available without special request — if it isn’t, the manufacturer doesn’t have it.

Color stability data. Initial Gardner color or APHA value. Yellowing index at full cure (ASTM E313). UV aging data — YI increase after defined accelerated UV exposure. Batch-to-batch color consistency data across at least 5 production batches.

Pot life at range of mixed masses. Standard 100g/150g laboratory data plus data at 1kg and 5kg mixed masses. Without this, wholesale buyers can’t accurately communicate pot life to professional fabricators working at commercial volume.

Raw material sourcing transparency. Named primary raw material suppliers, qualified supplier list, and raw material change notification policy. Color consistency across production runs is only achievable if raw material inputs are stable — and raw material stability requires documented supplier management.

OEM and packaging capability. Matched-component filling capability. Custom label production. Bilingual documentation capability. Minimum order quantities for OEM production that work for wholesale buyers at realistic launch volumes.

Export documentation. IMDG classification for both components, GHS-compliant SDS in destination-market format, UN-certified packaging, and Certificate of Analysis per shipment.

Jinhua Resin (jinhuaresin.com) is a Guangdong-based epoxy resin manufacturer producing deep pour epoxy formulations for professional furniture and commercial installation applications. Temperature rise data, color stability documentation, pot life across mixed masses, matched-component OEM packaging, and full export documentation are standard for wholesale buyers.


A Reference: Deep Pour Epoxy Specification Requirements by Buyer Segment

Buyer TypeVolume/OrderKey Spec RequirementsOEM Need
Custom studio5–50LClarity, color stability, tech supportLow
Production furniture brand100–500LBatch consistency, CoA, pour depth dataMedium
Contract manufacturer200–2,000LMax pour depth >75mm, temp-range data, color matchMedium–High
Private label brand200–1,000LFull OEM, custom packaging, bilingual docsHigh

The Professionalization Opportunity

The deep pour epoxy segment is in transition. Five years ago, most volume moved through craft channels to hobbyist buyers. Today, production furniture brands, hospitality contractors, and retail resin labels are buying at wholesale volumes and expecting industrial-grade supply chain support — consistent formulation, documented specifications, OEM capability, and reliable logistics.

The Chinese epoxy resin manufacturers who can serve this transition — who have the formulation depth to produce genuine deep pour products, the QC systems to deliver batch consistency at wholesale volume, and the OEM infrastructure to support private label brands — are a smaller subset than the field of suppliers who will claim to. For B2B buyers building businesses in this segment, the qualification work is the moat.


Sourcing deep pour epoxy wholesale for furniture production or private label? Jinhua Resin offers pour depth documentation, color stability data, matched-component OEM packaging, and wholesale supply programs for the professional furniture market: jinhuaresin.com

Epoxy Resin Shelf Life

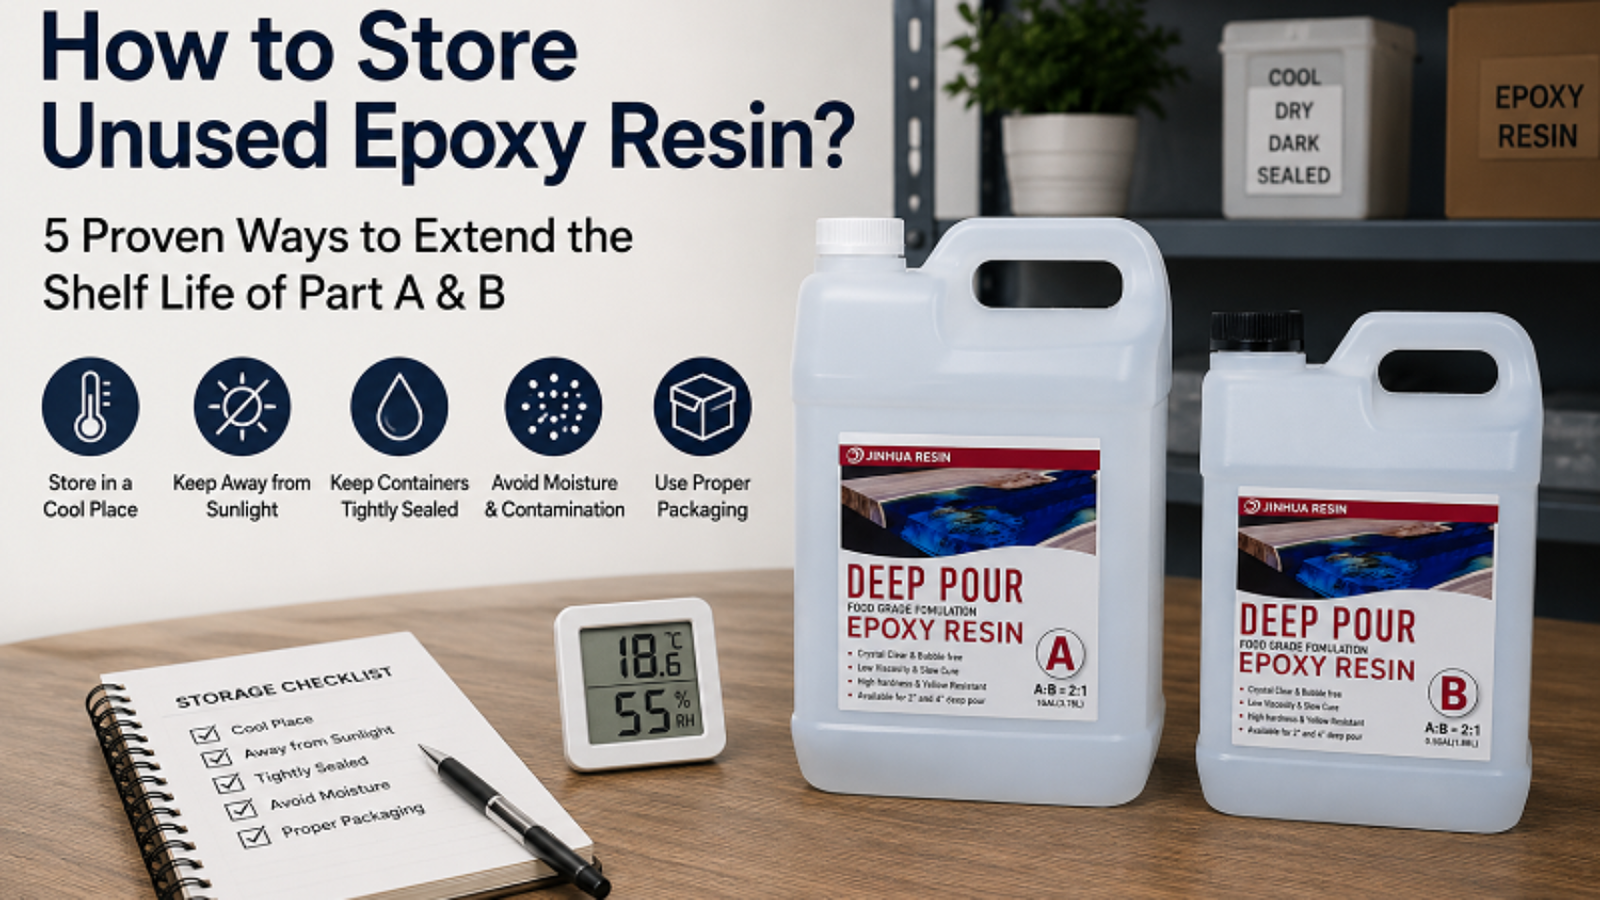
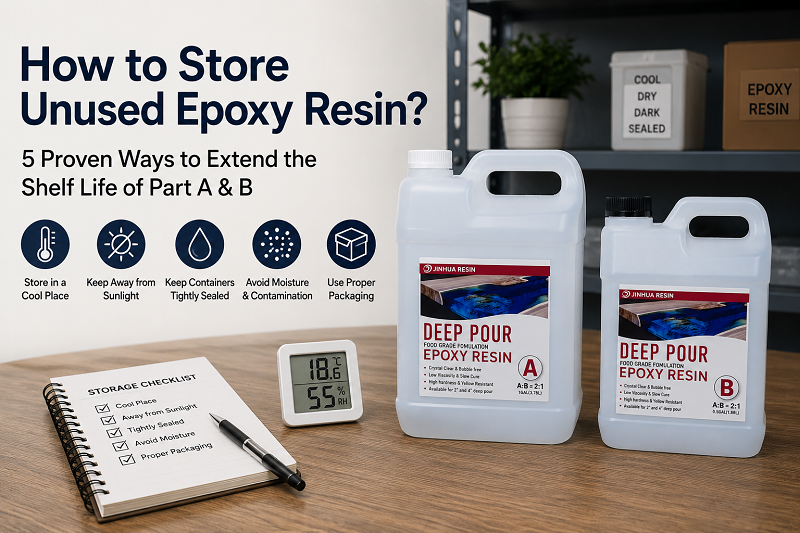
How to Store Unused Epoxy Resin? 5 Proven Ways to Extend the Epoxy Resin Shelf Life of Part A & B

Whether you rely on slow-reacting deep pour epoxy for massive timber castings or standard surface coats for countertops, epoxy remains a climate-sensitive compound. Almost every woodworker or resin artist has run into the same headache: opening a half-used bottle from months ago only to discover Part A turned into a milky, crystalline slush, or Part B aged into a dark amber color that fails to cure properly.

This isn’t just a waste of expensive raw materials; it can completely ruin a project you spent weeks preparing.

The good news? Unopened or partially used resin systems can easily maintain their performance for 12 to 24 months—provided you protect them from environmental hazards. Here is a breakdown of the silent culprits behind resin degradation and five practical rules to double your resin’s shelf life.

Epoxy Resin Shelf Life


What Ruins Unused Epoxy Resin?
Before you can store Part A and Part B properly, you have to understand what’s happening inside those bottles. Unmixed epoxy isn’t just sitting there—it’s constantly reacting to its environment.

  • Air & Moisture (The Hardener’s Worst Enemy): Part B hardeners love water. The second you leave the cap off, the liquid starts sucking humidity right out of the room. This triggers a chemical reaction called amine blushing, leaving you with amber-colored liquid, thick sludge, or a piece that stays sticky and foggy forever.
  • Sunlight & UV Rays: UV radiation tears apart the polymer chains in unmixed resin. Leave a clear bottle near a window, and it’ll turn yellow and brittle long before you even get a chance to mix it.
  • Wild Temp Swings: Summer heat bakes the liquid, triggering tiny thermal reactions inside the jug that kill its shelf life. On the flip side, winter cold freezes Part A into a solid, cloudy mess.

5 Rules to Keep Your Resin Fresh for Months

1. Keep the Room Temperature Steady (15℃-25℃)

If there is one thing liquid polymer hates, it’s a roller-coaster climate. Find a spot in your shop or house that stays consistently between 15℃ and 25℃.

  • Keep It Away from Heat: Don’t leave your stash in a hot summer garage, next to a radiator, or anywhere near direct sunlight. High ambient heat cooks the chemical batch, aging it months ahead of time.
  • Busting the Winter “Freeze” (Crystallization): If your workspace drops below 10℃, Part A might look like milky white slush or turn completely rock-hard. Don’t panic and don’t throw it away. It hasn’t gone bad; it just crystallized. Tighten the cap, submerge the bottle in a warm water bath (50℃-60℃) for 30 to 60 minutes, and watch the crystals melt right back into liquid glass.

    2. Lock Out Air (Seal Immediately & Use Inert Gas Barriers)
    Air exposure is the main reason amine hardeners turn yellow and lose their reactivity.

    Wipe Threads & Cap Instantly: After pouring what you need, wipe the bottle threads clean with a dry paper towel to prevent the cap from gluing shut, then tighten the lid immediately.

    Pro Hack for Half-Empty Jugs: When using large containers of deep pour resin, pouring out half leaves a massive air gap inside the jug. Spraying a quick burst of inert heavy gas (like Argon or specialized resin preserver spray) into the container before capping creates an invisible blanket over the liquid, displacing moisture and oxygen.

    3. Block UV Light: Say No to Clear Bottles
    Direct light compromises the optical clarity of your raw materials.

    Always store your compounds inside their original opaque containers (usually high-density polyethylene or metal cans).

    If you transfer liquid into smaller working bottles for daily use, choose dark amber or opaque squeeze bottles and tuck them inside a closed cabinet away from windows.

    4. Never Mix Up Caps or Dispensing Tools
    Cross-contamination is an easy mistake that ruins entire batches.

    Part A and Part B caps often look identical. If you accidentally swap them, residual chemicals on the inside of the cap will trigger a tiny localized cure along the threads, forming hard crusts or contaminating the whole jug.

    The Fix: Mark your “A” and “B” lids clearly using bold, different-colored markers. Never use the same stir stick or pump for both components.

    5. Practice FIFO & Smart Decanting
    Label Everything (The FIFO Rule): As soon as a box arrives at your shop, slap the date on the bottle with a Sharpie. Write down when it arrived and the exact day you popped the seal. Always reach for the oldest bottle on the shelf first—opening a fresh jug when you still have half-used stock sitting around is just asking for expired chemicals.Don’t Keep Cracking the Main Jug: Buying deep pour resin in bulk gallons saves money, but opening a massive container just to grab a few ounces for a small coaster project is a huge mistake. Every time you open that lid, fresh, humid air rushes in. Instead, pour off a small working batch into smaller, airtight squeeze bottles for daily use. That way, your main stash stays factory-sealed and fresh for the big builds.
    Final Thoughts
    Epoxy resin isn’t a non-perishable product; think of it as a reactive liquid that demands careful handling. By controlling temperature, air exposure, light, and cross-contamination, you can ensure your unused Part A and Part B remain crystal clear, fully reactive, and ready for your next build—even a year down the road.
Table Top Epoxy

Crystal Clear Every Time: How Manufacturers Control Clarity and Eliminate Bubbles in Table Top Epoxy

The Problem That Shows Up Three Days After the Pour

A woodworker pours a river table. The pour looks clean — no visible bubbles, good color, self-leveling nicely. Three days later, full cure reveals a haze across the center panel, a cluster of micro-bubbles just below the surface, and a faint yellow tint that wasn’t there in the liquid. The wood is fine. The technique was fine. The table is a reject.

This scenario plays out constantly in the table top epoxy segment, and the root cause attribution is almost always wrong. The customer blames technique. The distributor suspects the customer. The manufacturer defends the product. In most cases, the actual problem is a combination of formulation characteristics and application conditions that nobody in the chain explained clearly at the point of sale.

For B2B buyers sourcing table top epoxy for resale or private label, understanding what drives optical clarity — and what drives bubble formation — is not just technical knowledge. It’s the difference between a product that generates repeat orders and one that generates support calls.

Table Top Epoxy

Optical Clarity: What It Is and What Degrades It

“Crystal clear” is a marketing phrase. In manufacturing terms, optical clarity in cured epoxy resin is measured through three distinct properties, each with a different cause and a different solution when it goes wrong.

Yellowness Index (YI)

Yellowing is the most common clarity complaint in table top epoxy. It manifests as a warm amber tint in the cured resin, ranging from barely perceptible to strongly discolored depending on the formulation and the conditions under which it cured.

The primary cause of initial yellowing — yellow color present immediately after cure, before any UV exposure — is the hardener chemistry. Aromatic amine hardeners (including DETA, TETA, and similar compounds) are inherently yellowing. They’re reactive and fast, which is why cheap commodity epoxy often uses them, but they produce a colored cure. Cycloaliphatic amine hardeners and modified aliphatic systems cure to a substantially cleaner color. A table top epoxy formulated with non-yellowing hardener chemistry starts clear; one formulated with aromatic amines starts amber.

Secondary yellowing — color development over time with UV exposure — is a separate mechanism. Even a non-yellowing hardener system will yellow under sustained UV exposure without adequate photoprotection. UV stabilizer packages (hindered amine light stabilizers, or HALS, combined with UV absorbers) slow this process. The concentration and selection of these additives is a formulation decision; it doesn’t show up on the product label and requires direct inquiry with the manufacturer.

What to ask:

  • What hardener chemistry does the formulation use — aromatic, aliphatic, or cycloaliphatic amine?
  • What is the initial Yellowness Index at full cure (ASTM D1925 or ASTM E313)?
  • What UV stabilizer package is included, and what is the expected color retention under defined UV exposure conditions?

Haze and Cloudiness

A cured epoxy that looks clear in a thin section but shows haze or cloudiness in a thicker pour, or when viewed at an angle, has a scattering problem — light is being deflected by microscopic structures within the polymer matrix rather than passing through cleanly.

There are several sources of this scattering:

Incomplete mixing. Epoxy resin and hardener that aren’t thoroughly combined cure inhomogeneously — some regions richer in resin, some richer in hardener. These composition gradients create refractive index variations that scatter light. This is a user technique issue but also a formulation issue: higher-viscosity products are harder to mix completely, and products with narrow mixing ratios (where a small measurement error produces a large stoichiometric deviation) are less tolerant of imprecision.

Phase separation from moisture. Amine hardeners react with atmospheric moisture and CO₂. In humid conditions, this can cause blushing — a white, waxy surface layer — or internal cloudiness from moisture-induced phase separation. Formulations with moisture-tolerant hardener systems are significantly more robust in real-world application conditions.

Incompatible additives. Pigments, dyes, or other additives that aren’t fully compatible with the resin system can migrate, aggregate, or phase-separate during cure, creating localized cloudiness. This matters for any private label brand adding colorants to a clear base resin — the compatibility of the colorant system with the base needs to be validated, not assumed.

Residual stress in thick sections. In deeper pours that generate significant exothermic heat, thermal stress during cure can create micro-fractures or density variations in the polymer that scatter light. This is why deep pour products and table top products are distinct formulations — and why using a table top epoxy in a deep pour application produces both thermal and optical problems.

Surface Finish Quality

A perfectly clear epoxy can still look wrong if the surface finish is poor — fish-eyes, orange peel texture, or a matte rather than gloss surface. Surface finish is partly a formulation characteristic (surface tension, flow-out behavior, defoamer presence and concentration) and partly an application condition issue (substrate contamination, temperature during pour, overly aggressive torching).

The defoamer question is worth exploring directly with the manufacturer. Defoamers reduce surface tension and help air escape from the mixed resin during the working time window. Under-defoaming leaves micro-bubbles. Over-defoaming causes fish-eye craters. Getting the concentration right for a given viscosity and working time is a formulation optimization — and it’s one of the less visible variables that distinguishes a product developed for table top applications from a general-purpose casting resin.


Bubble Formation: Causes, Types, and Control

Bubbles in cured epoxy are not all the same. They form through different mechanisms, at different stages of the application process, and require different interventions. Knowing which type you’re dealing with determines whether the solution is a formulation change, a process change, or a user education change.

Mixing Bubbles

The act of combining Part A and Part B introduces air. Mixing too vigorously — especially with a drill mixer at high speed — whips air into the resin the way a whisk aerates cream. These bubbles are typically small and uniformly distributed through the mixed resin.

Most table top epoxy formulations have sufficient working time and low enough viscosity for mixing bubbles to self-degas — the bubbles rise to the surface and pop under their own buoyancy during the working time window. Formulations with higher viscosity, shorter working time, or insufficient defoamer don’t degas adequately, and the mixing bubbles become permanent.

What this means for sourcing: Viscosity at application temperature and working time are the two formulation specs most predictive of self-degassing performance. A product with 800–1,200 cPs at 25°C and 30+ minutes working time will self-degas reliably. A product with 2,500 cPs at 20°C and 20 minutes working time will not.

Substrate Outgassing

Wood — particularly freshly cut, green, or porous species like oak and walnut — outgasses moisture and air when warm resin is applied. The heat from the mixed resin, combined with the temperature differential between the resin and the wood, drives gas out of the substrate and into the resin layer from below.

These bubbles typically appear 10–30 minutes after the pour, rising from the wood surface upward. They’re often larger and more localized than mixing bubbles, and they can’t be fully addressed by torching — more bubbles keep coming as the outgassing continues.

The standard professional practice is a seal coat: a thin, brushed application of epoxy to the substrate before the flood coat, allowed to cure to the point where outgassing is complete before the flood coat is applied. The seal coat traps the outgassed air in the thin cured layer rather than letting it migrate into the flood coat.

For private label brands, this application guidance needs to be in the product documentation. Customers who don’t know about seal coating will blame the product for substrate outgassing bubbles.

Recoat Bubbles

In multi-layer applications, bubbles can form at the interface between a cured first coat and a second pour. The cause is usually one of two things: the first coat has fully cured and a hard barrier has formed that traps air between layers, or solvent cleaning between coats introduced contamination that disrupts surface tension.

The recoat window — the time after the first coat during which a second pour will chemically bond without adhesion issues — is a product-specific specification. Most table top epoxy products have a recoat window of 4–24 hours after the first pour; outside this window, mechanical preparation (light sanding) is required before recoating.

This specification is frequently missing from product TDS sheets. If your product doesn’t specify the recoat window, request it from the manufacturer — and if they don’t have data on it, treat that as a formulation gap.


The Formulation Variables That Actually Matter

Sourcing table top epoxy for resale means making formulation choices that affect end-user outcomes. These are the variables worth interrogating at the manufacturer level.

Viscosity at application temperature. Lower viscosity means better self-leveling, better self-degassing, and better penetration into wood grain on the seal coat. Products in the 800–1,500 cPs range at 22–25°C are the practical sweet spot for table top applications. Viscosity above 2,000 cPs at room temperature requires more deliberate degassing technique from the end user.

Pot life vs. working time. Covered elsewhere in this series, but relevant here: longer working time gives bubbles more time to rise and self-degas before the viscosity increases enough to trap them. Products with 30–40 minutes working time at standard conditions are more forgiving than products with 15–20 minute windows, all else equal.

Hardener type and its color contribution. As discussed, cycloaliphatic or modified aliphatic hardeners for non-yellowing cure. This is not negotiable for a premium table top product — aromatic amine hardeners will always produce a yellower cure.

UV stabilizer package. HALS + UV absorber combination at adequate concentration for the product’s intended outdoor and window-adjacent applications. The formulation should specify expected color retention performance — yellowing index increase over a defined UV dose.

Defoamer type and concentration. Not visible on TDS sheets but directly affects surface finish and bubble performance. Ask whether the formulation uses a silicone or non-silicone defoamer — silicone defoamers can interfere with certain topcoat adhesion applications and may not be appropriate for all use cases.

Self-leveling additives. Some formulations include flow-leveling additives that improve surface finish without requiring a perfectly level substrate. Relevant for professional installers doing on-site pours.


Questions to Ask Your Table Top Epoxy Manufacturer

On clarity:

  • What hardener chemistry does the formulation use, and what is the measured Yellowness Index at full cure?
  • What UV stabilizer package is included? What is the expected YI increase after accelerated UV exposure testing (ASTM G154 or equivalent)?
  • Has the formulation been tested for haze or cloudiness in pours at 3mm, 6mm, and 12mm depth?

On bubbles:

  • What is the viscosity at 20°C, 23°C, and 25°C?
  • What defoamer type and concentration is used?
  • Does the formulation self-degas when mixed at low speed? At what working time and temperature?
  • Is there documented data on substrate outgassing behavior with common wood species?

On application guidance:

  • What is the recommended recoat window for second-layer pours?
  • Is seal coat application recommended, and if so, what are the recommended seal coat parameters?
  • At what ambient temperature range is the formulation designed to perform?

Jinhua Resin (jinhuaresin.com) is a Guangdong-based epoxy resin manufacturer producing table top epoxy formulated specifically for clarity-critical applications. Non-yellowing hardener chemistry, UV stabilizer packages with documented color retention performance, optimized defoamer concentration, and full TDS documentation including viscosity data across temperature range are standard for all table top epoxy product lines.


A Formulation Spec Reference for Table Top Epoxy Buyers

PropertyTarget RangeWhy It Matters
Viscosity (Part A, 25°C)800–1,500 cPsSelf-leveling and bubble release
Working time (25°C)30–45 minTime for bubbles to self-degas
Initial Yellowness Index< 2.0 (ASTM E313)Color quality at cure
Hardener typeCycloaliphatic or modified aliphaticNon-yellowing cure
UV stabilizerHALS + UV absorberLong-term color retention
Recoat window4–24 hoursMulti-layer application guidance
Shore D hardness (full cure)75–85Surface durability

The Clarity Problem Is Mostly a Documentation Problem

The majority of clarity and bubble complaints in the table top epoxy segment are not caused by defective products. They’re caused by products that perform well within their design parameters but are used outside those parameters — wrong ambient temperature, wrong substrate preparation, wrong mixing technique, wrong recoat timing — because the documentation didn’t explain the parameters clearly enough.

For B2B buyers, this is an opportunity. A supplier who can provide clear, specific, application-condition documentation — not just a TDS with physical property numbers, but actual guidance on seal coats, recoat windows, temperature ranges, and mixing technique — gives their distribution customers a product that works reliably in the field. That reliability is what generates the second order, the third order, and the referral.

The formulation matters. The documentation matters equally.


Sourcing table top epoxy for distribution or private label? Jinhua Resin provides non-yellowing formulations with documented clarity performance, UV stability data, and full application guidance for all table top epoxy product lines: jinhuaresin.com